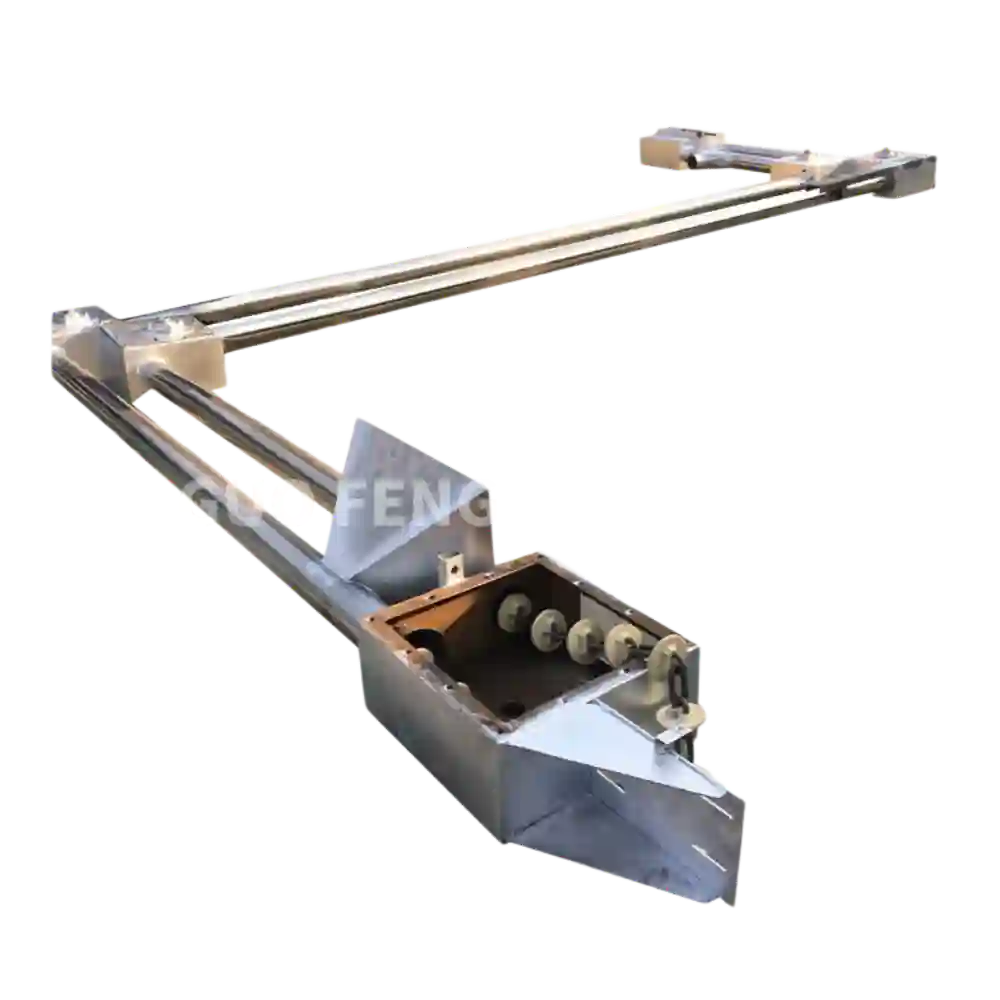
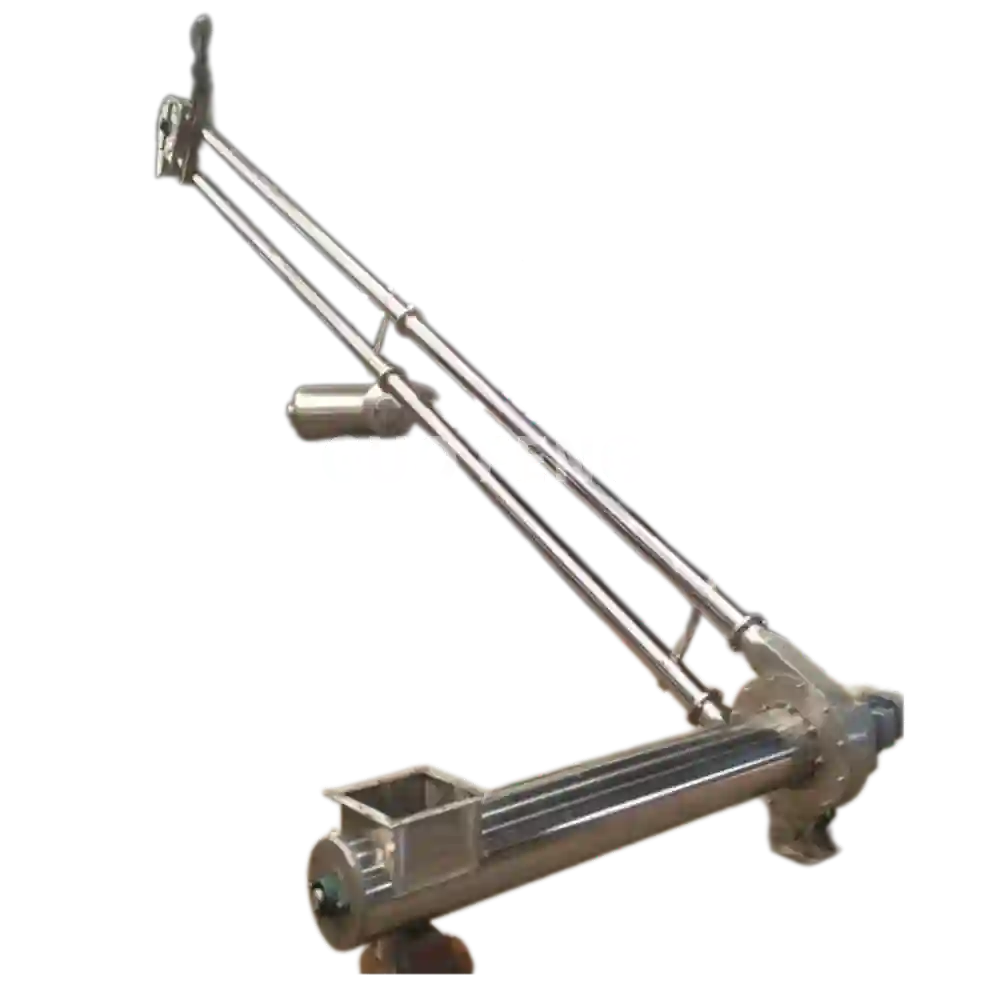
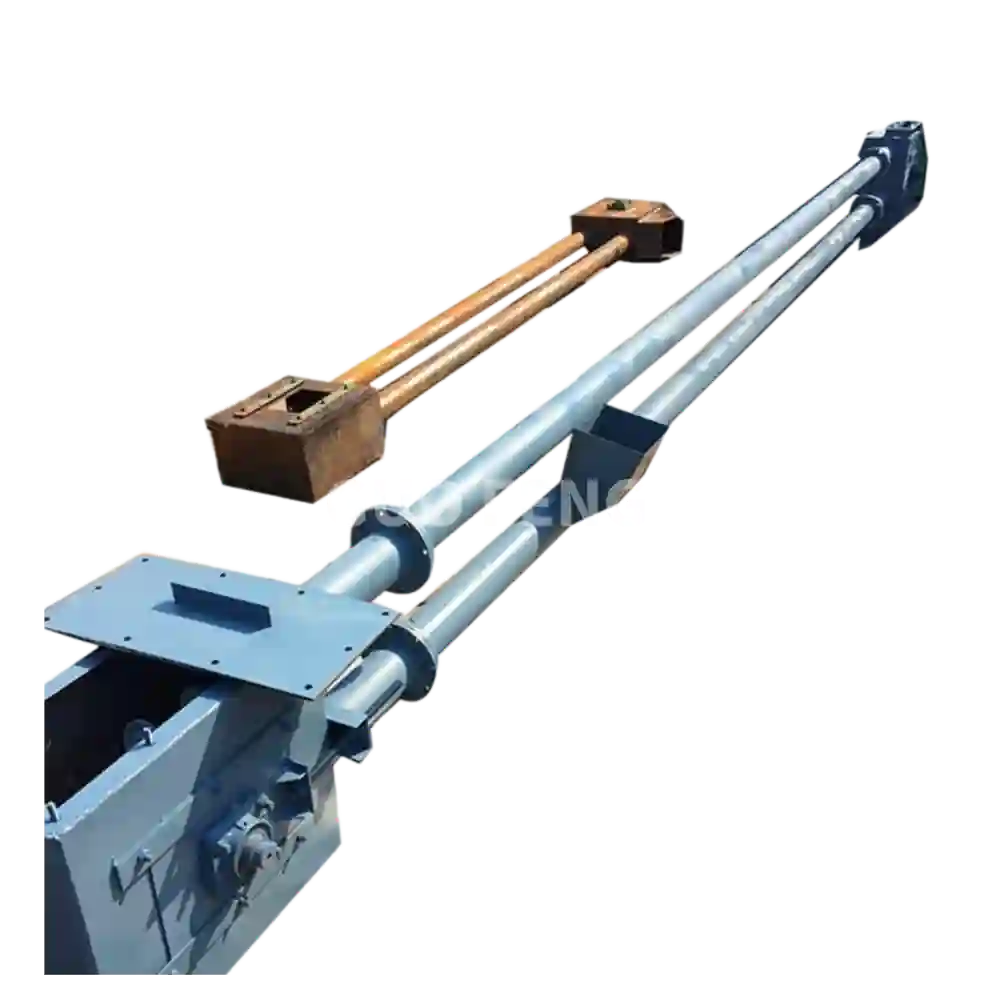
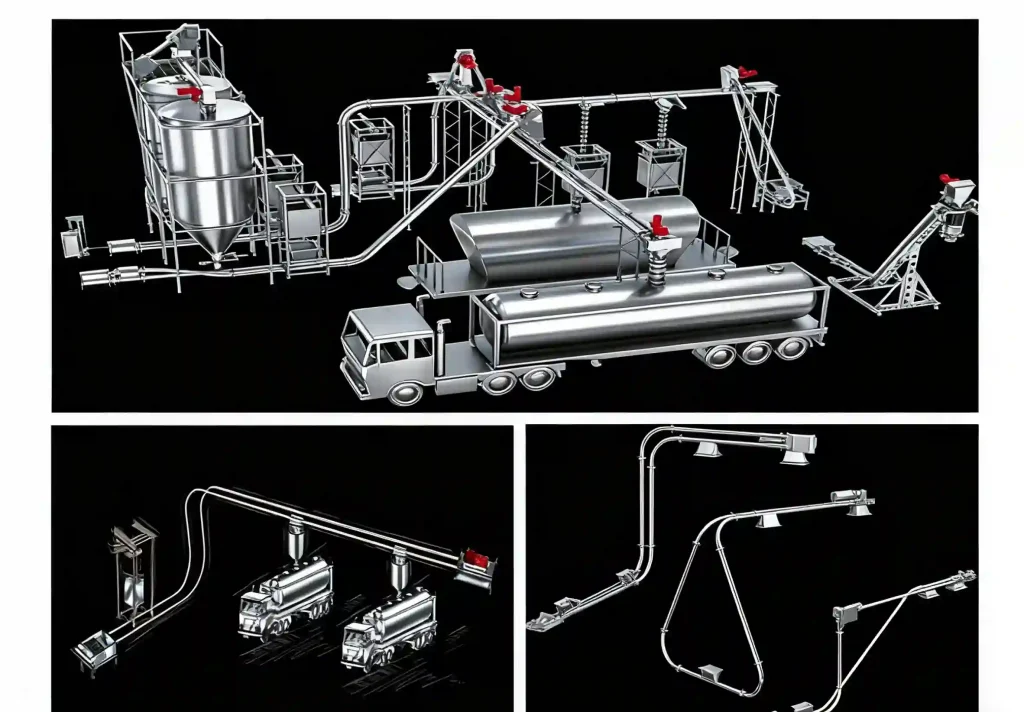
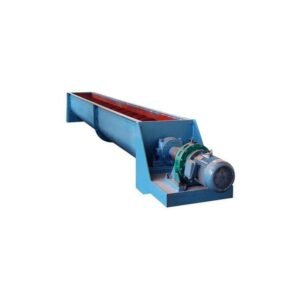
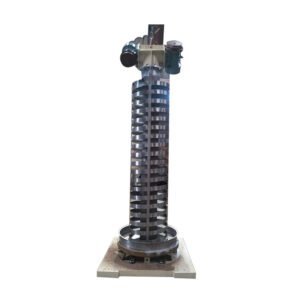
Application Areas: Dust-tight conveying of powders and granules. Widely used in chemicals (polyurethane pellets), food (flour, starch, FDA-compliant), pharmaceuticals (API intermediates, GMP), and minerals (titanium dioxide powder). Ensures zero dust emission, gentle material handling, and flexible multi-directional conveying.
Particle Size Range
Motor Power
Capacity
Suitable for conveying powders, granules, and bulk materials such as: polyurethane pellets, flour, starch, pharmaceutical powders, titanium dioxide, cement, fly ash, and other fine chemical or mineral raw materials. Ensures gentle handling and prevents material damage or contamination.
Widely used in food, chemicals, pharmaceuticals, and minerals industries. Ideal for applications requiring dust-tight conveying, GMP-compliant clean environments, and flexible multi-directional layouts. Ensures zero dust emission, energy efficiency, and safe conveying across long distances.
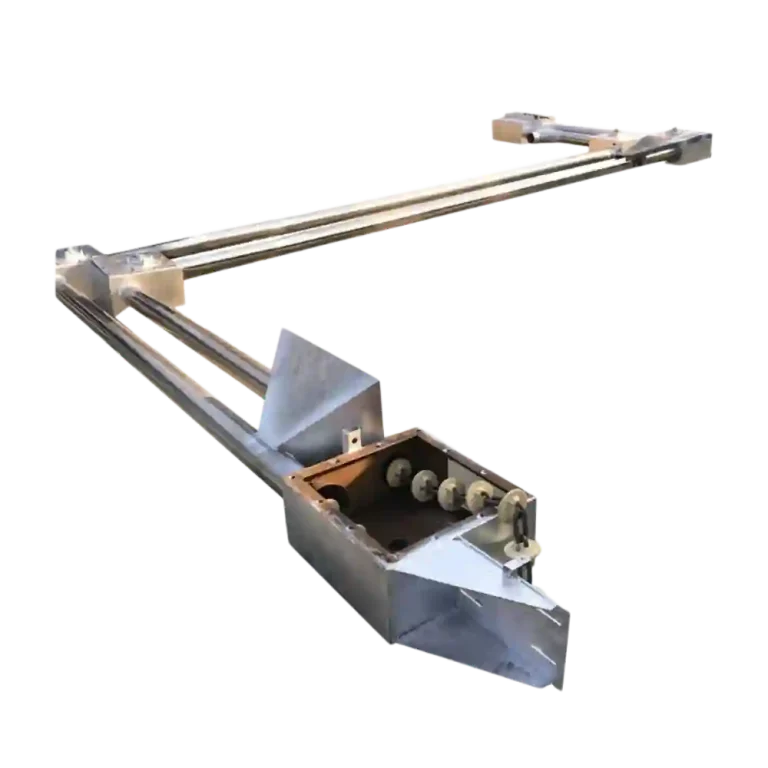
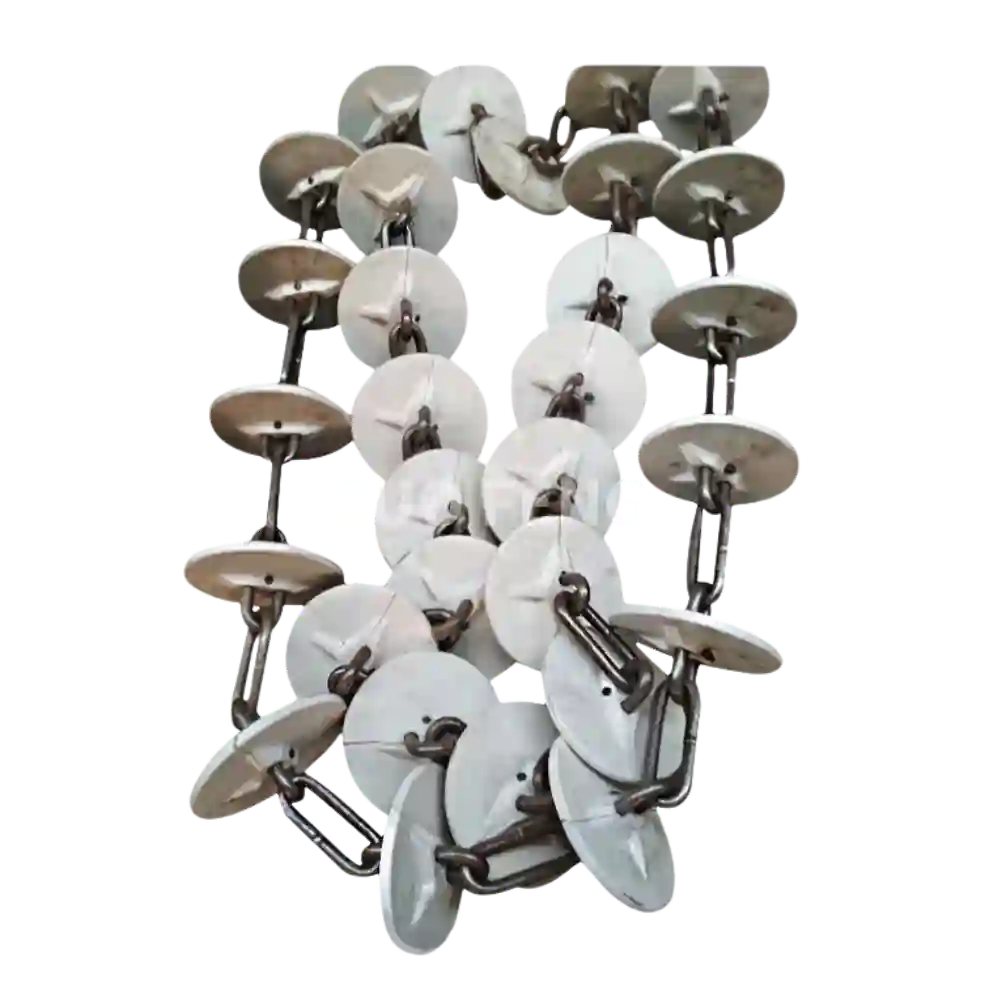
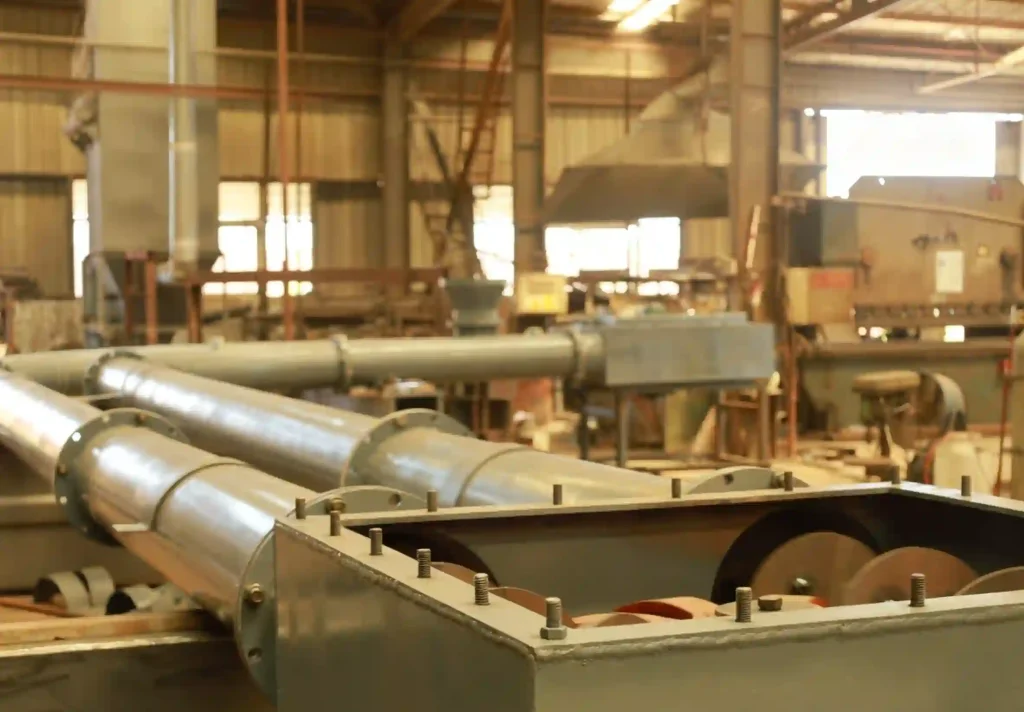
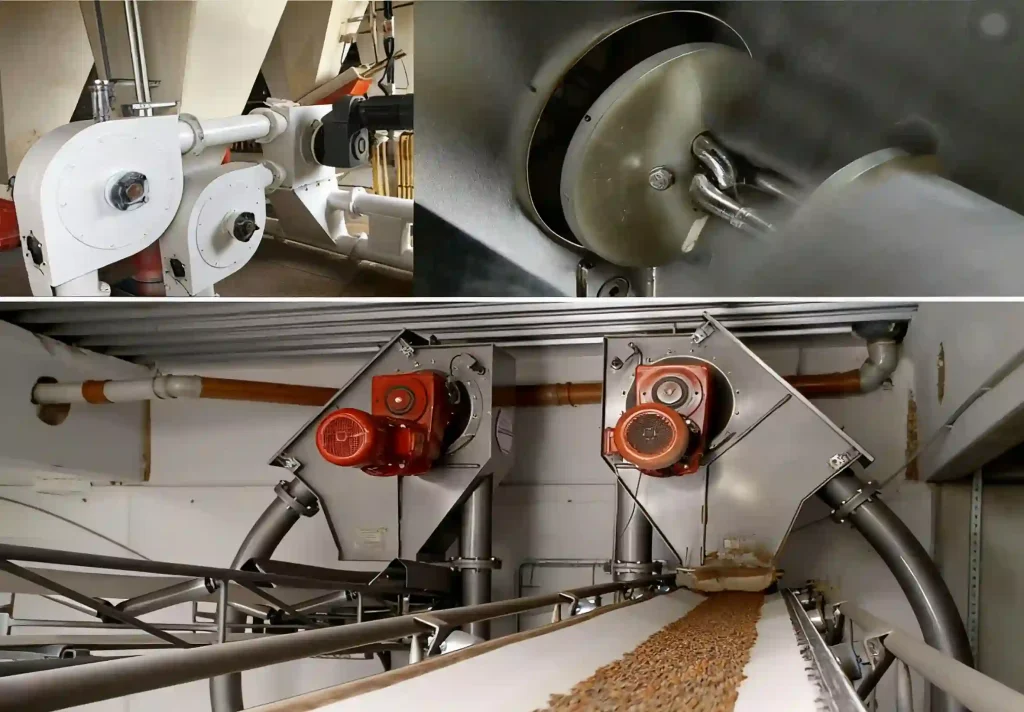
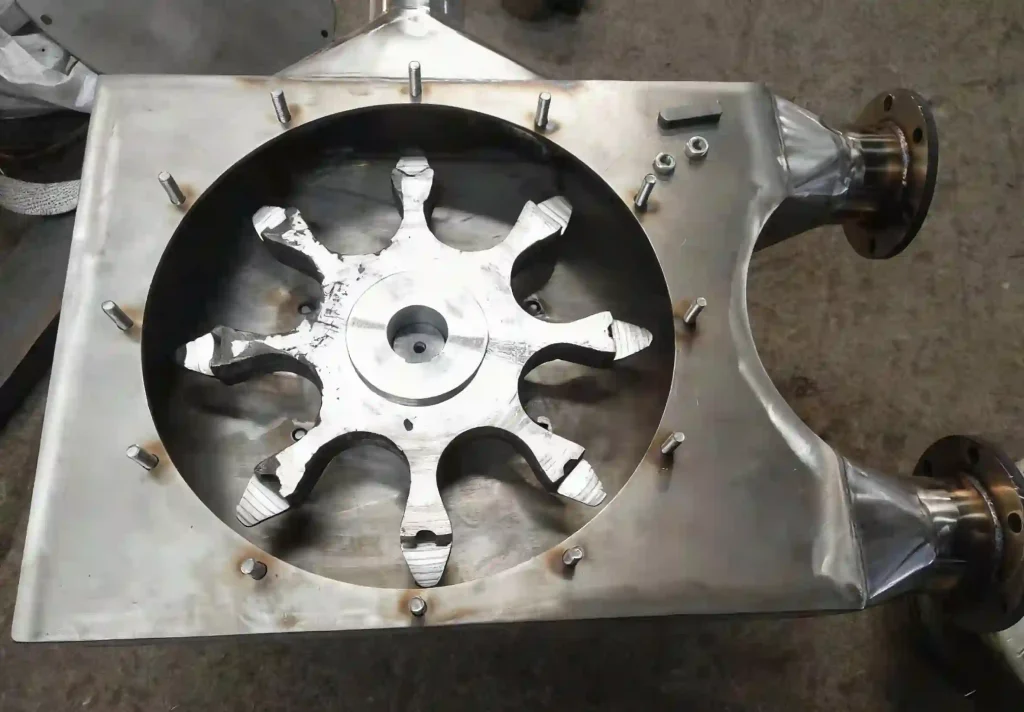
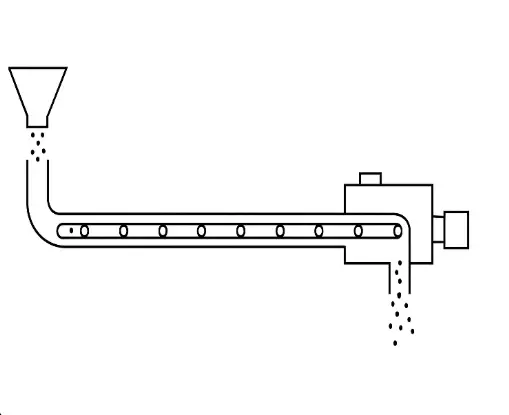
The Tubular Drag Chain Conveyor is a fully enclosed system designed for dust-tight conveying of powders and granules. Inside the circular tube, a continuous chain with disc attachments gently drags material through the pipeline, ensuring minimal degradation and supporting multi-directional transport (0–90° inclinations).
With IP66-rated seals to eliminate dust emissions, <0.1% product degradation (SGS-verified), and chain life exceeding 20,000 hours (ISO 281 certified), it provides both reliability and efficiency. The system is widely used in chemicals (polyurethane pellets), food (flour, starch), pharmaceuticals (API intermediates), and minerals (titanium dioxide powder), ensuring clean, safe, and flexible bulk material handling.
The tubular drag chain conveyor is an efficient enclosed conveying system that uses a continuous chain to move bulk materials through a sealed tube. It ensures dust-tight and safe operation, suitable for handling powders, granules, and fragile materials. The system not only provides reliable conveying performance but also offers a 25% energy efficiency improvement, significantly reducing power consumption. With ultra-low product degradation (<0.1%, SGS certified) and extended chain service life (20,000+ hours, ISO 281 verified), it ensures stable and long-term operation. The modular structure allows multi-directional conveying (horizontal, vertical, and inclined) within one system, saving installation space and reducing layout complexity. Additionally, its anti-leakage and anti-contamination design make it widely applicable in industries such as food, chemicals, pharmaceuticals, and minerals, meeting strict hygiene and safety requirements.