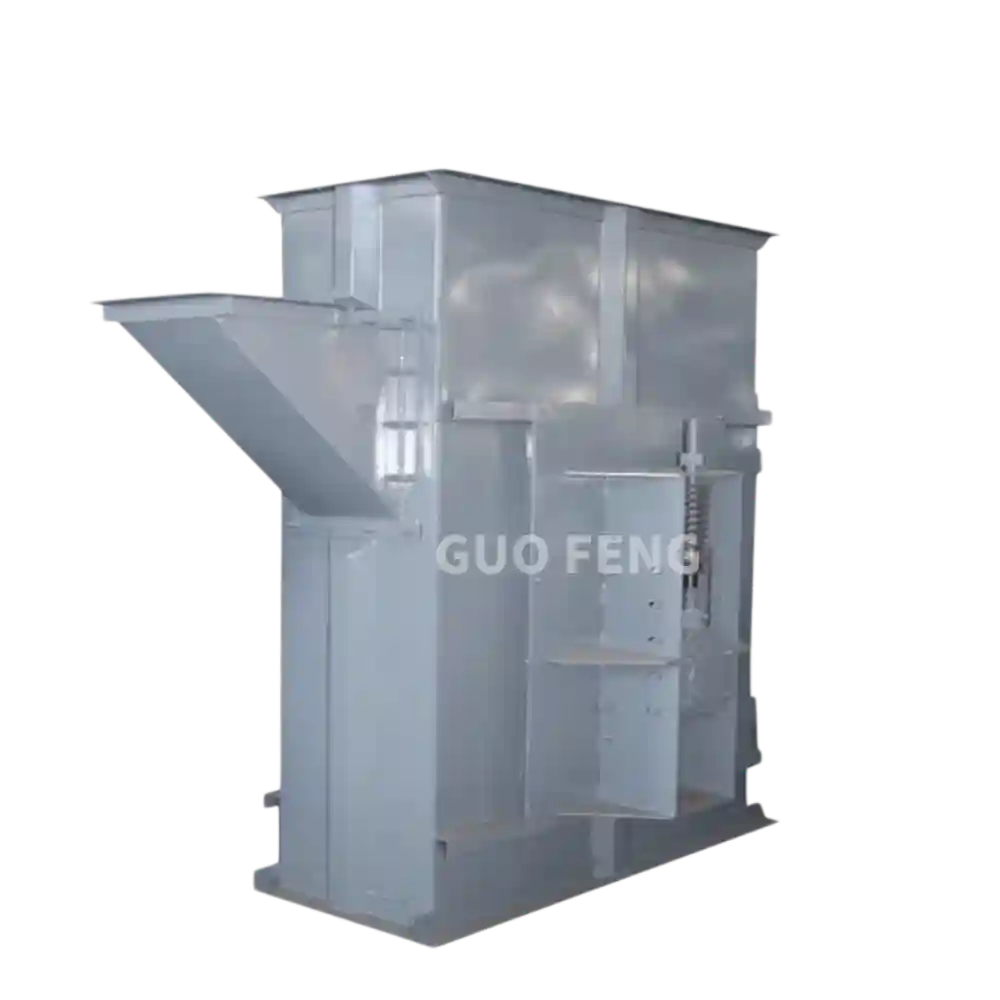
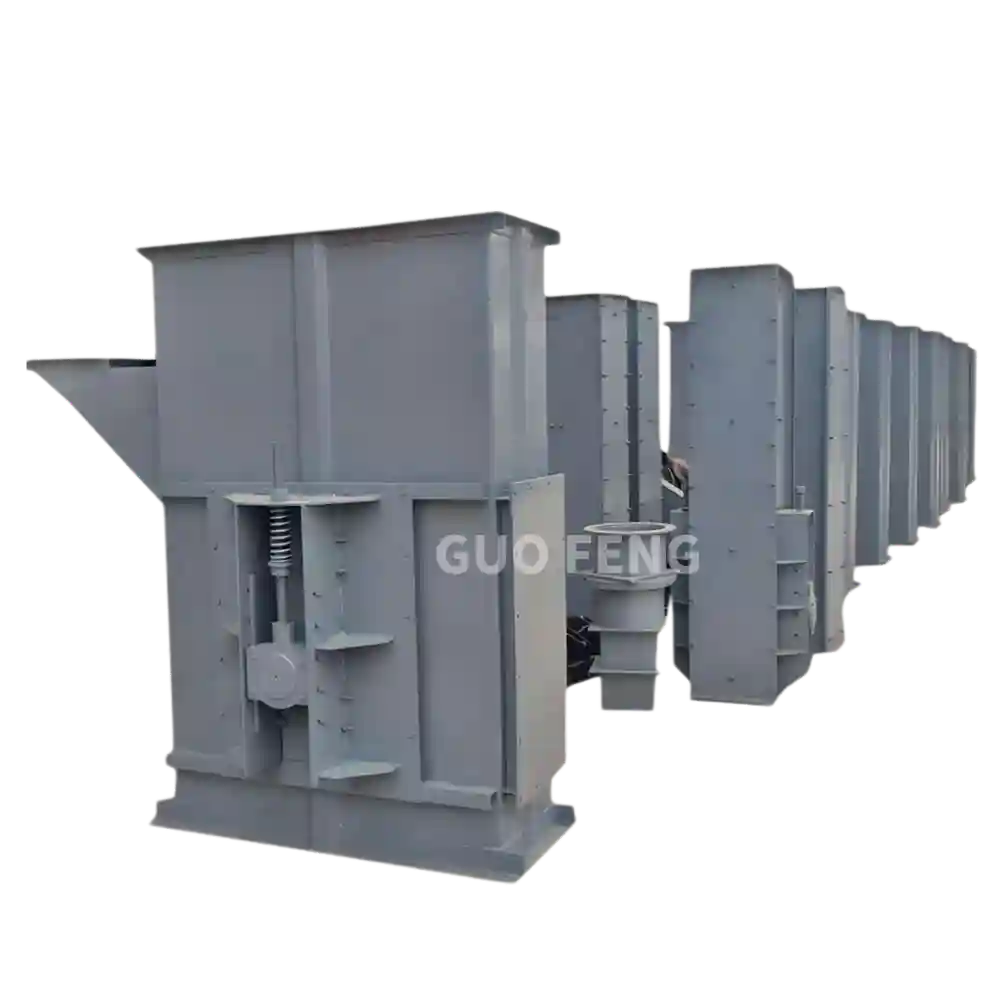
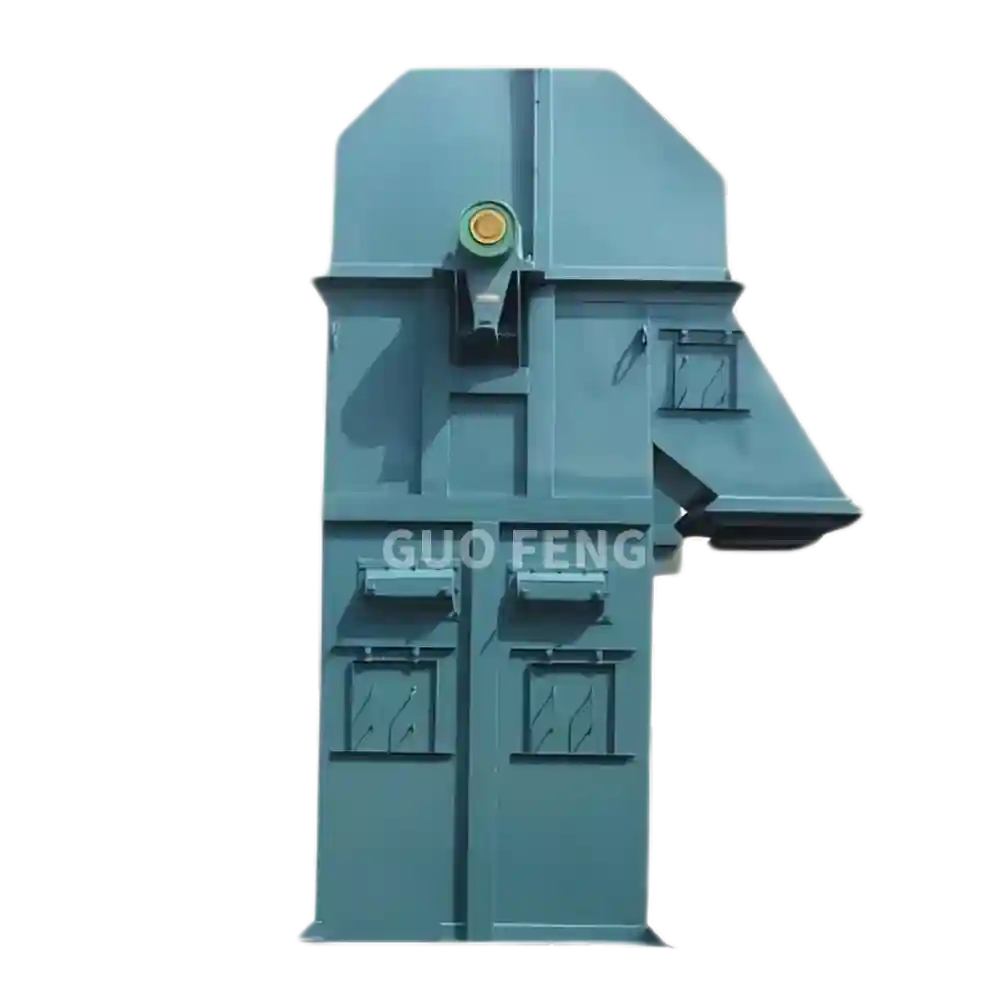
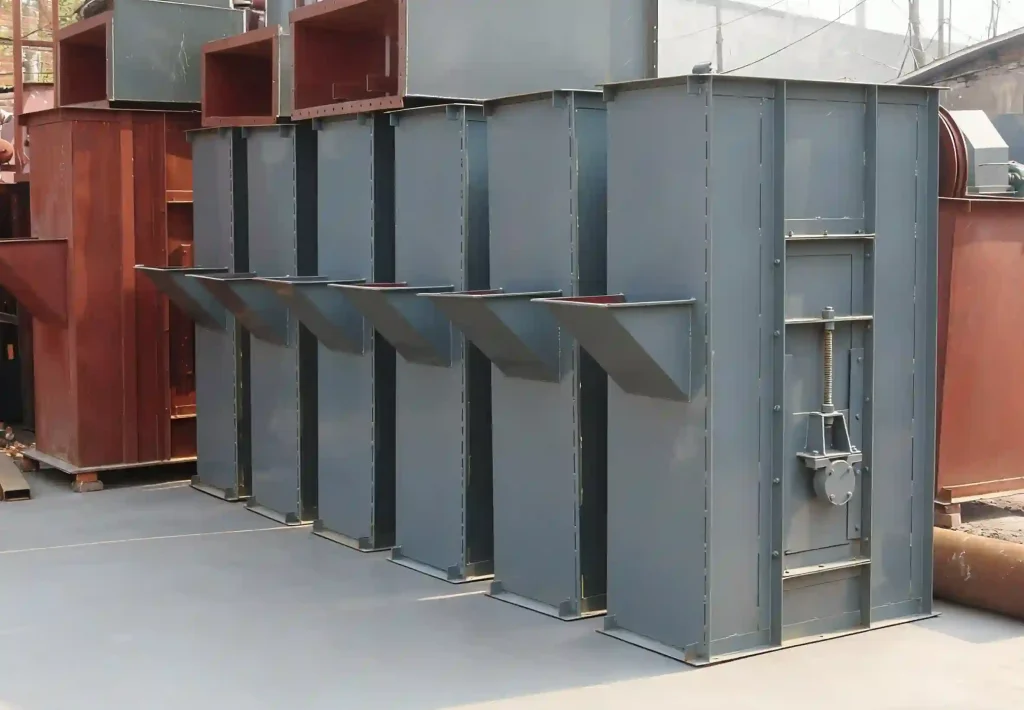
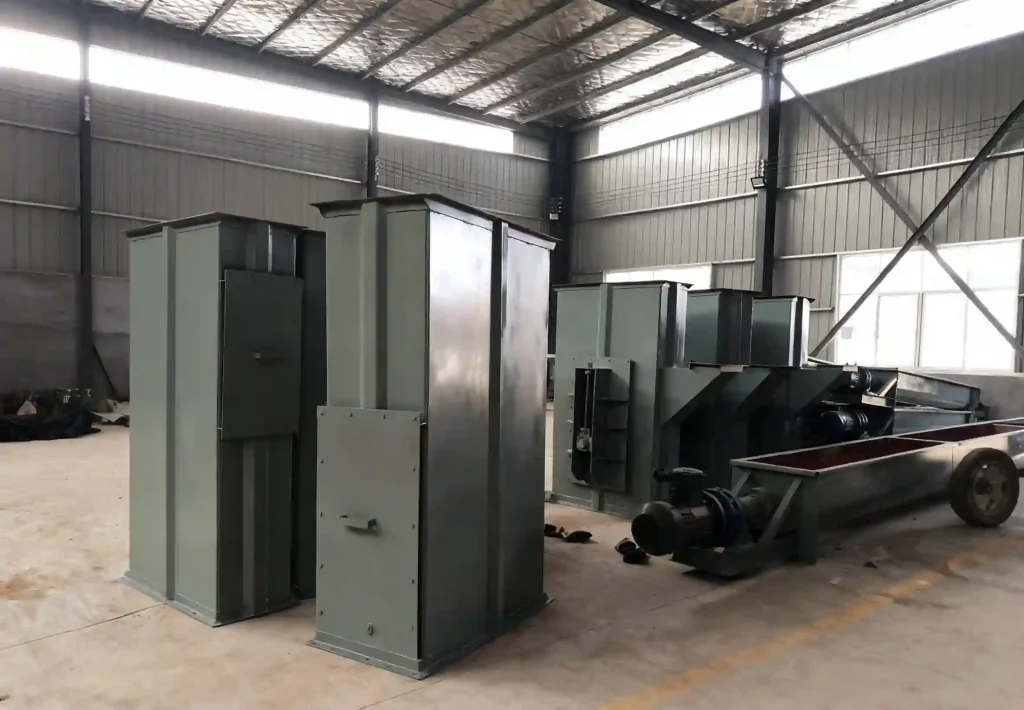
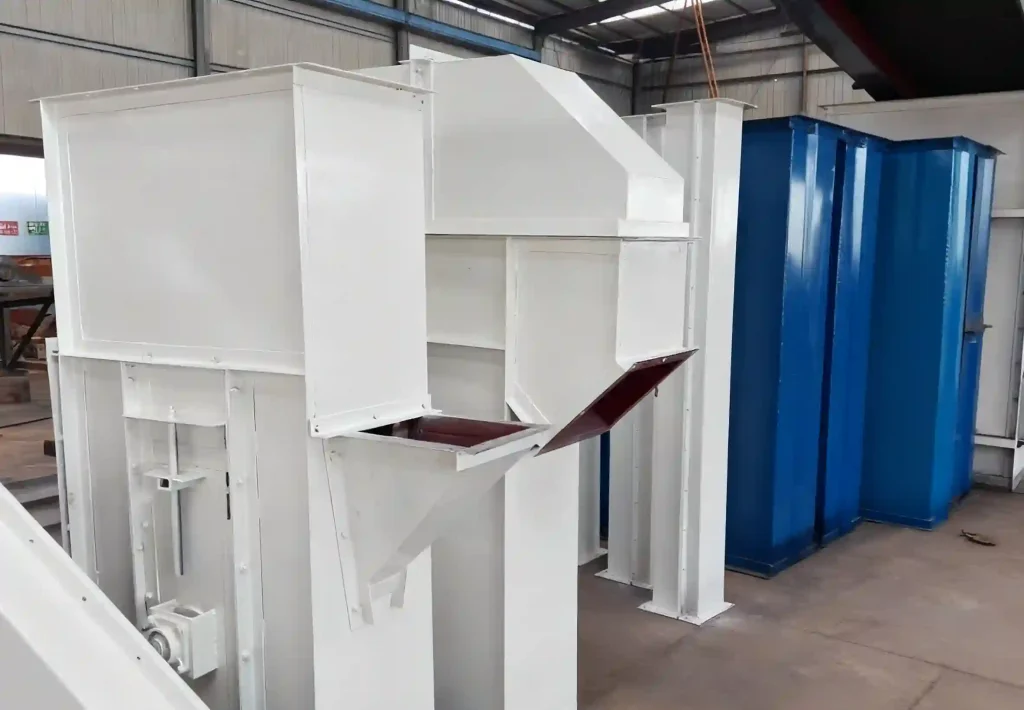
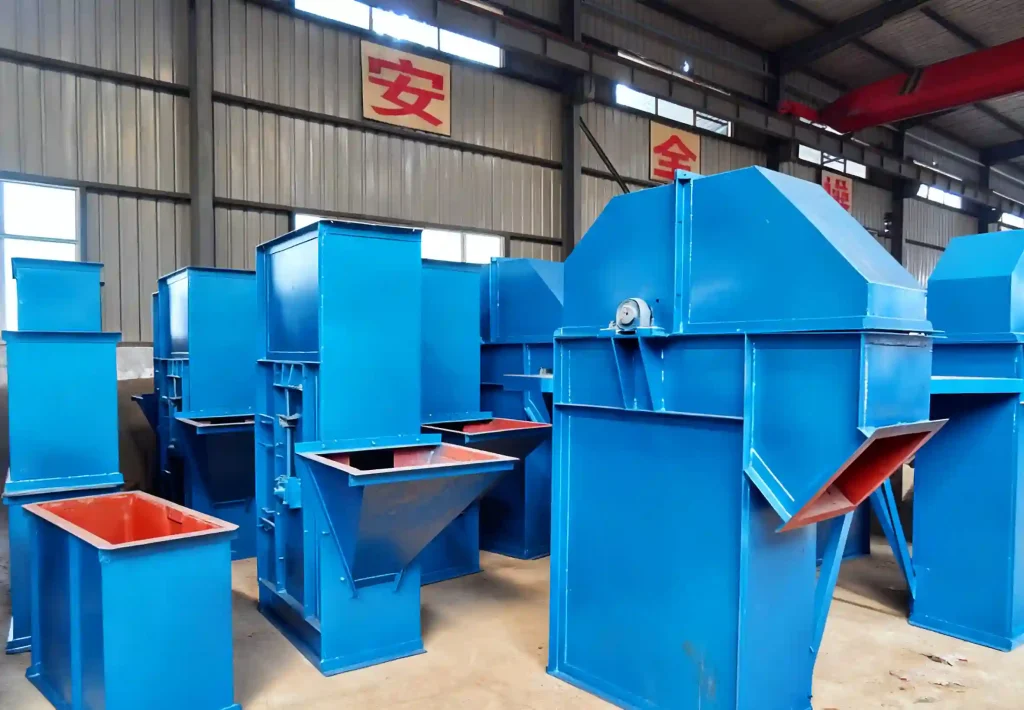
Application Areas: Continuous vertical lifting of powders, granules, and small lumps (≤60°C). Widely used in cement (clinker conveying), grain (silo filling), mining (ore hoisting), coal (power plant fuel handling). Centrifugal discharge ensures efficient material release with <0.5% residue.
Material Temperature
Belt Speed
Compared to chain elevators
The TD Belt Bucket Elevator is suitable for powders, granules, and small lumps of bulk materials with low abrasiveness and material temperature ≤60°C. Typical materials include cement powder, coal, grain, fertilizer, sand, and other fine to medium bulk solids.
Mainly applied in cement plants (clinker and cement powder conveying), grain storage silos (wheat, corn, rice, etc.), power stations (coal handling), and mining & chemical industries (ore, fertilizer, non-abrasive minerals). Designed for continuous vertical lifting with stable capacity and low power consumption.
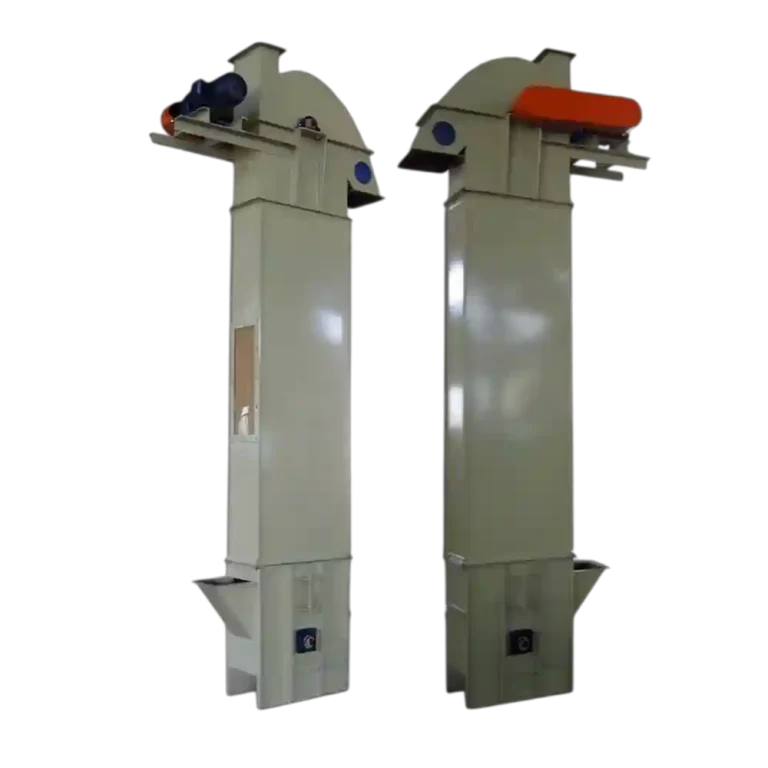
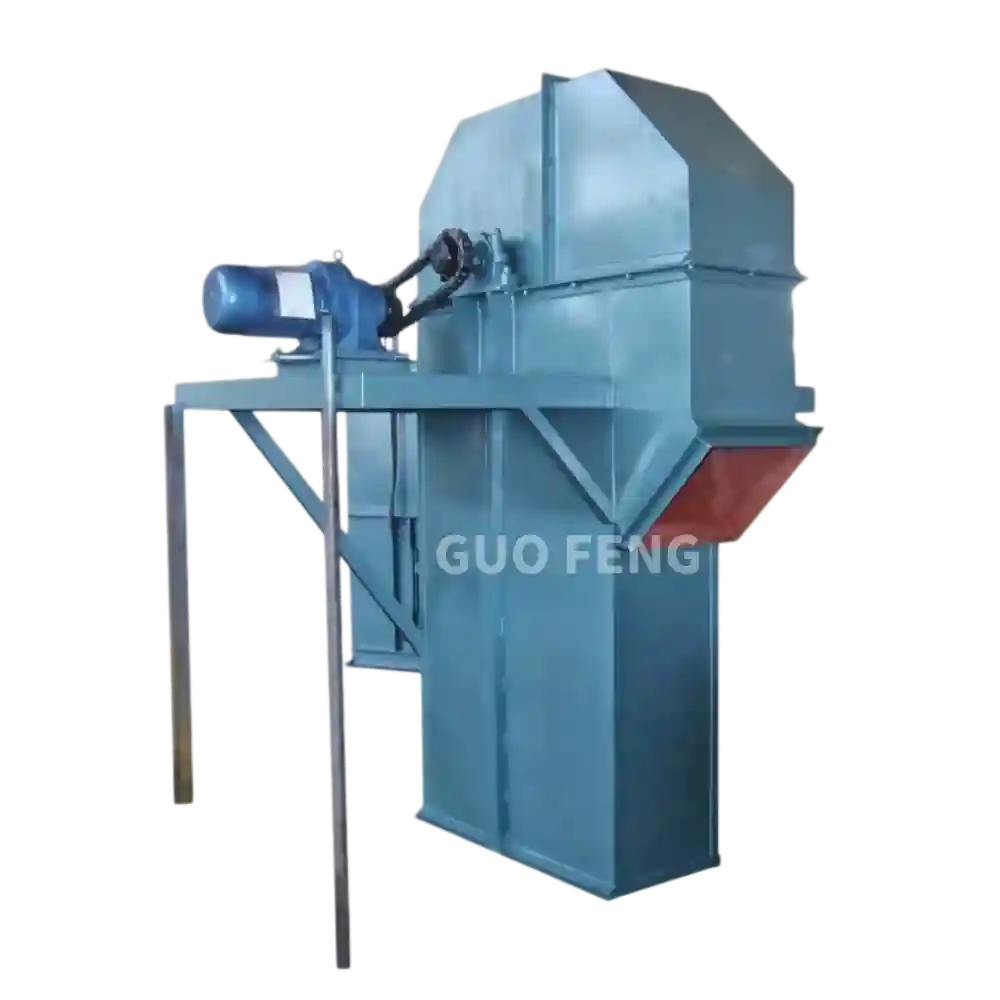
The TD Belt Bucket Elevator is a continuous vertical lifting equipment designed for powders, granules, and small lumps with material temperatures up to 60°C. It adopts a rubber belt as the traction component, with buckets evenly fixed on the belt to carry materials upward at a speed of 1.4–2.0 m/s.
Featuring centrifugal discharge at the head section, it ensures efficient unloading with minimal material residue (<0.5%). The structure is simple, with low power consumption, smooth operation, and easy maintenance, making it highly reliable for long-term operation.
This series is widely applied in cement (clinker, cement powder), grain (wheat, corn, rice, silo filling), power stations (coal handling), and chemical industries (fertilizer, non-abrasive minerals).
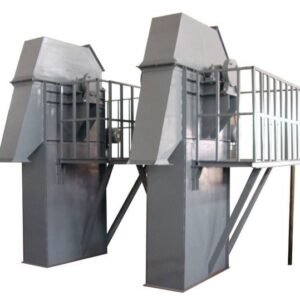
The TD Belt Bucket Elevator is a highly efficient vertical conveying device that uses a rubber belt with evenly spaced buckets to continuously lift bulk materials. Its simple and compact structure ensures stable operation, low noise, and easy maintenance, making it suitable for long-term industrial use.
Compared with chain-type elevators, the TD belt design provides 40% higher conveying efficiency while significantly reducing power consumption. The centrifugal discharge method ensures smooth material unloading with minimal residue (<0.5%).
Additionally, the belt bucket elevator features lightweight construction, reduced dynamic load, and lower operational costs, making it ideal for handling powders, granules, and small lumps in cement, grain, coal, and chemical industries.
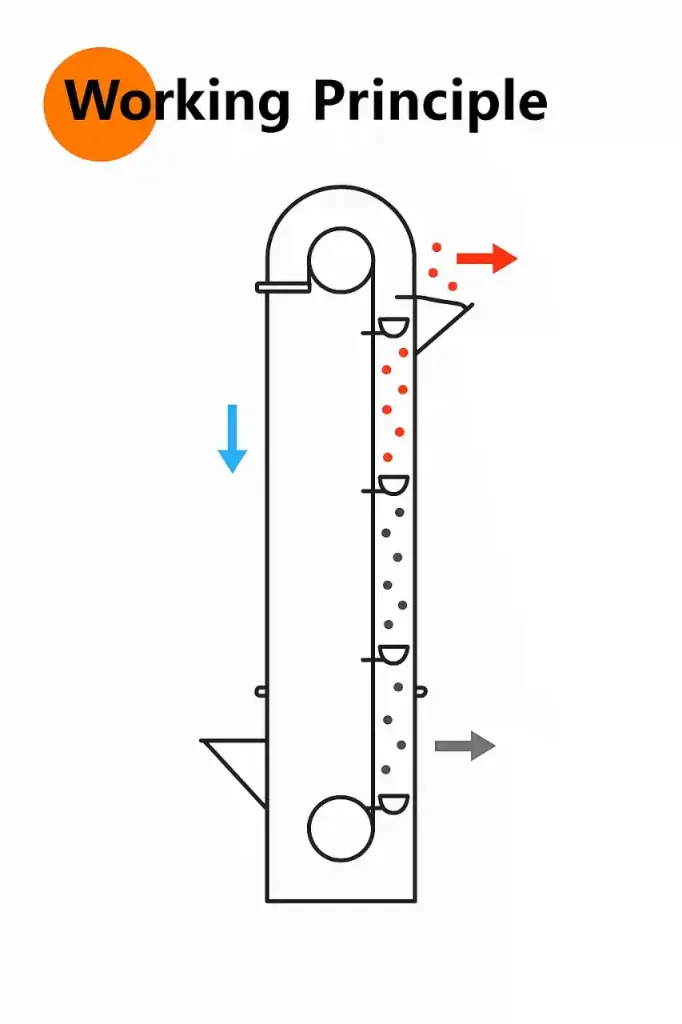
The TD Belt Bucket Elevator operates with a rubber belt as the traction component, on which buckets are evenly fixed. During operation, the belt runs at a speed of 1.4–2.0 m/s, carrying bulk materials vertically upwards.
At the head section, materials are discharged through centrifugal force, ensuring smooth unloading and minimal residue. The bottom section collects materials from the feed inlet, which are continuously scooped up by the buckets and transported upward.
This design enables continuous vertical lifting of powders, granules, and small lumps with stable performance, low power consumption, and high efficiency, making it widely used in cement, grain, coal, and chemical industries.