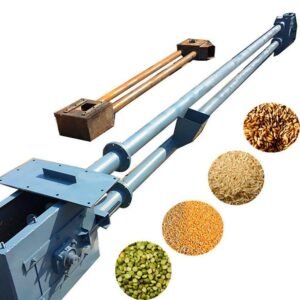
Application Areas: Bi-directional conveying of powders and granules up to 50 mm. Widely used in minerals (e.g., silica sand), food (grain, flour – HACCP compliant), chemicals (polymer pellets), and pharmaceuticals (powder intermediates – GMP compliant). Ensures gentle handling with <0.5% product degradation (SGS-verified). Compact footprint, dust-tight design, suitable for continuous upward or downward conveying.
Particle Size Range
Motor Power
Capacity
Bi-directional conveying suitable for powders and granules up to 50 mm. Ensures gentle handling with <0.5% product degradation (SGS-verified). Applicable to materials such as: silica sand, grains, flour, polymer pellets, pharmaceutical powders, etc.
Mainly used in minerals, food, chemicals, and pharmaceuticals. Typical applications include silica sand vertical transfer, grain and flour elevation (HACCP), polymer pellet conveying, and pharmaceutical powder intermediate transfer (GMP).
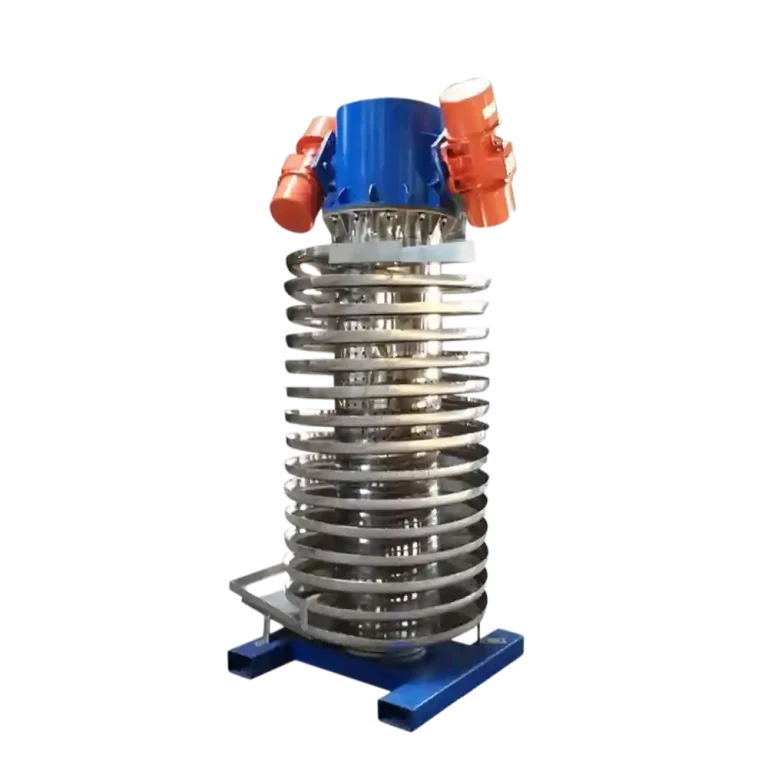
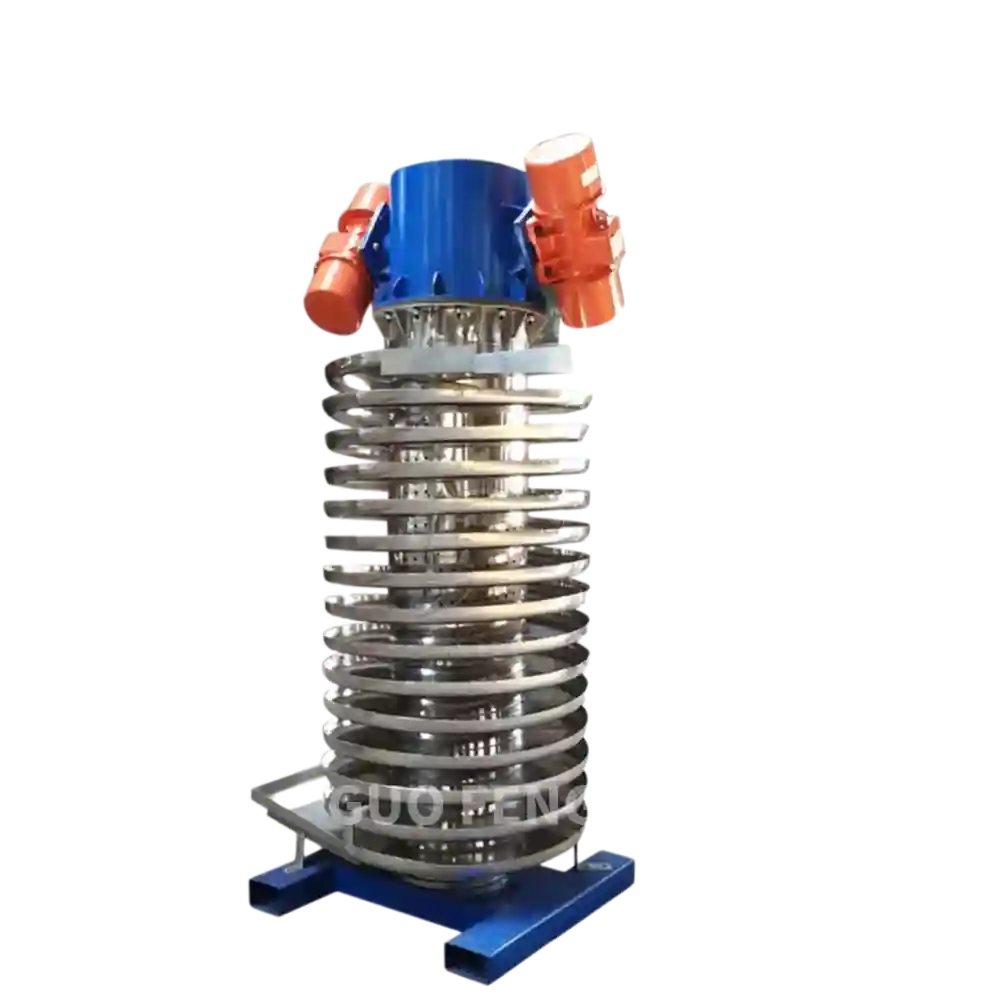
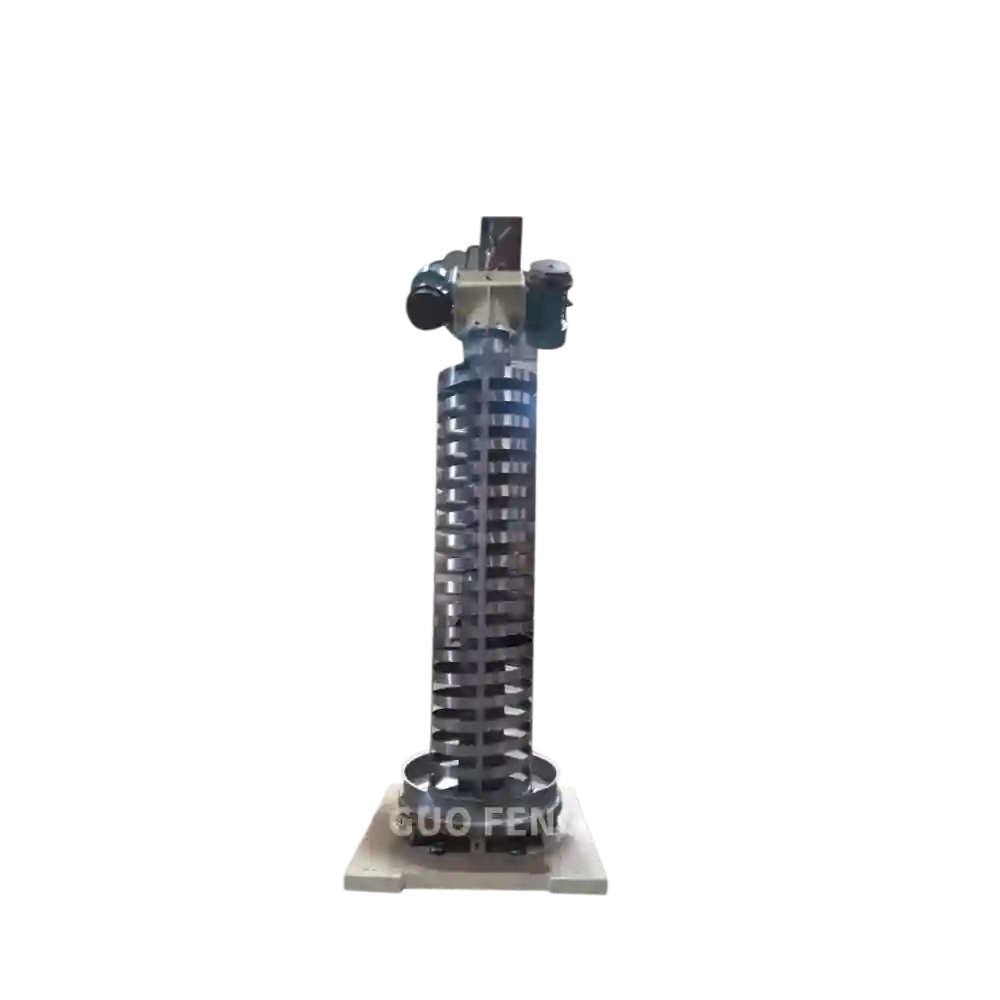
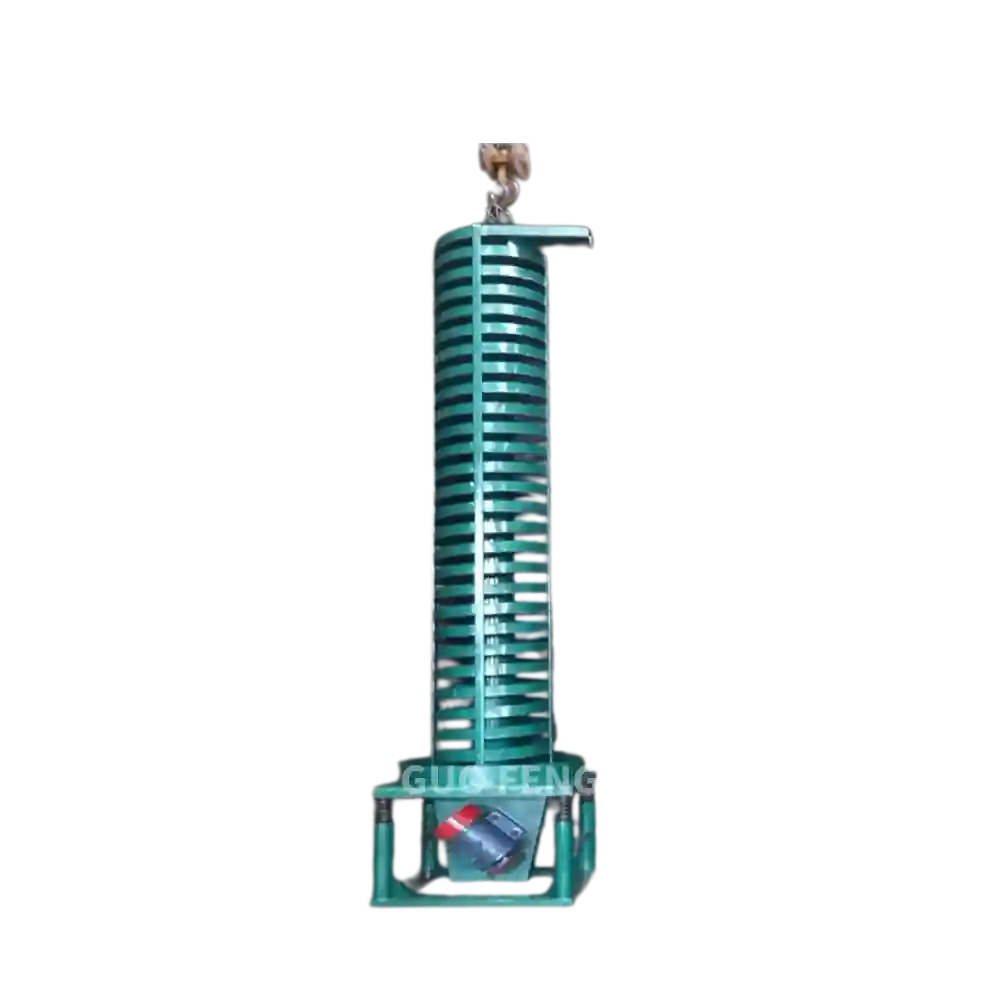
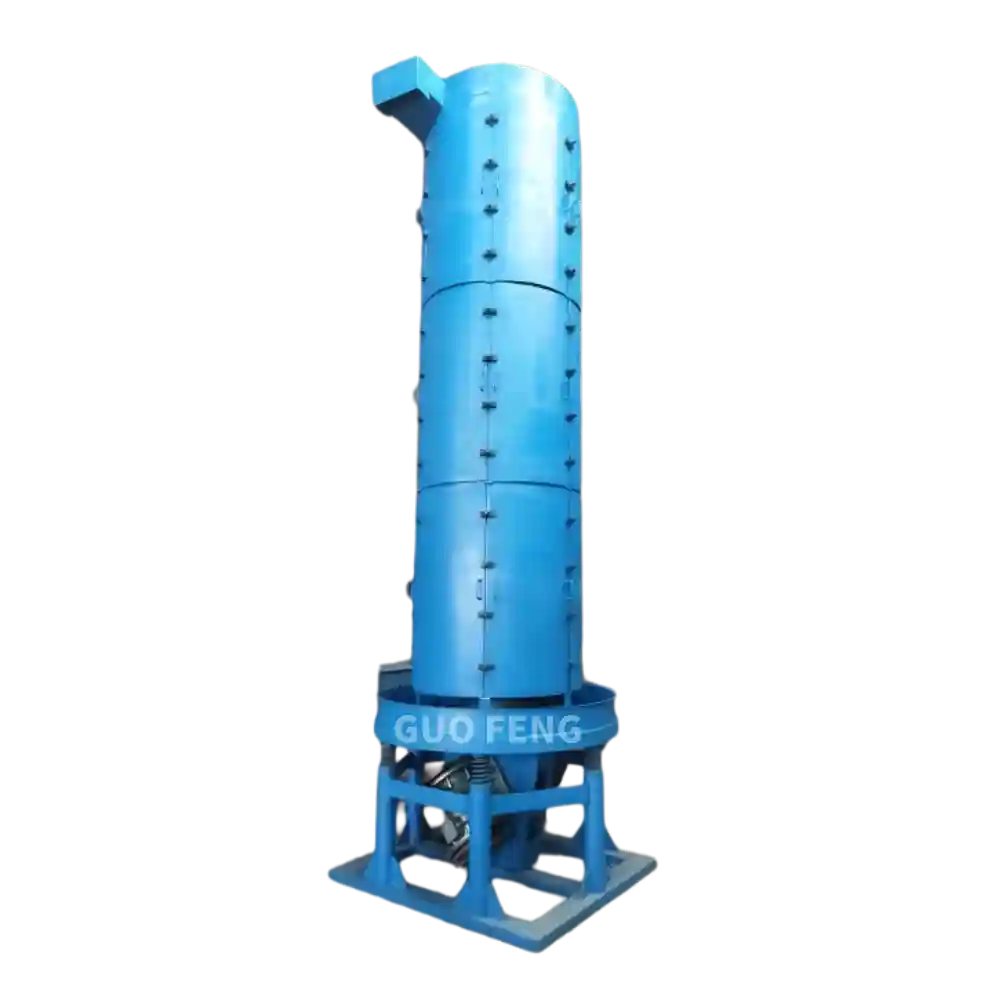
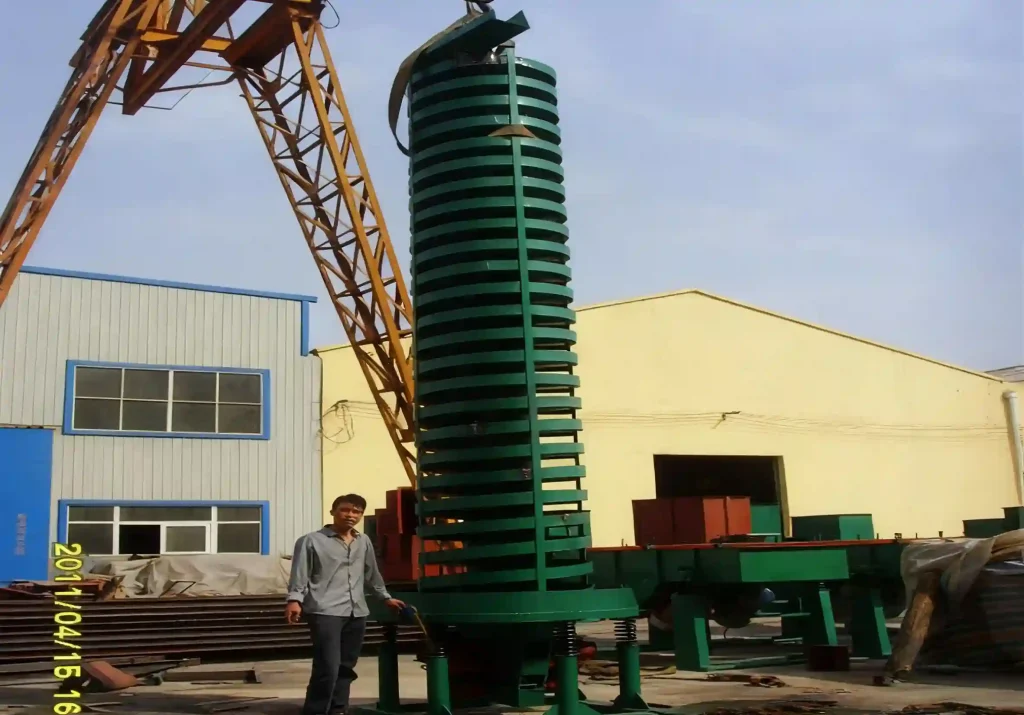
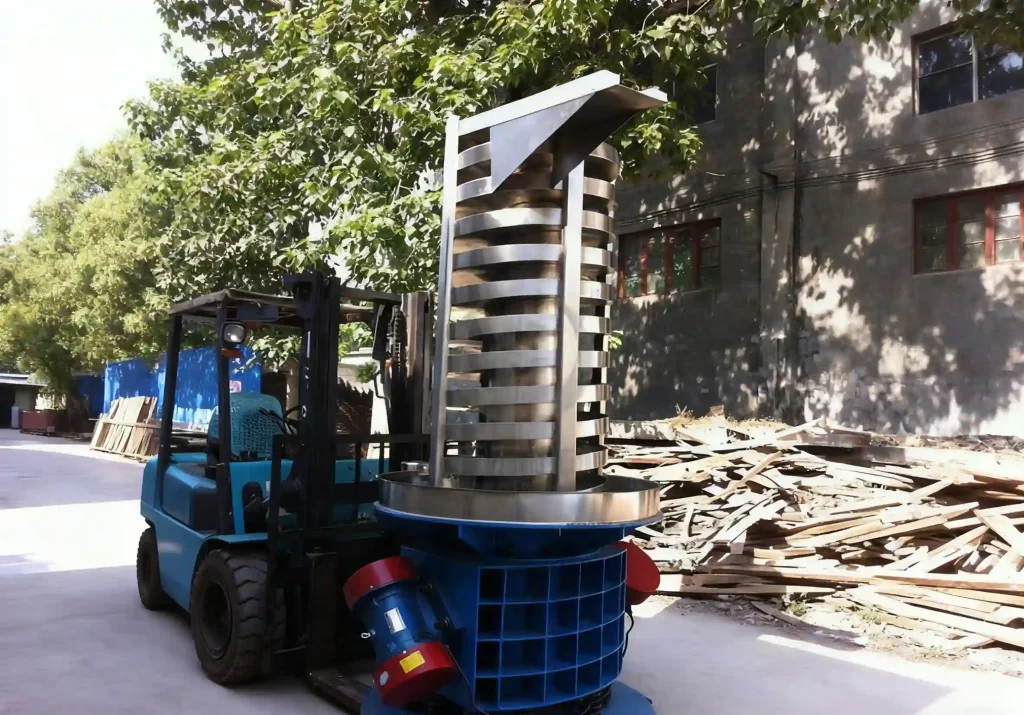
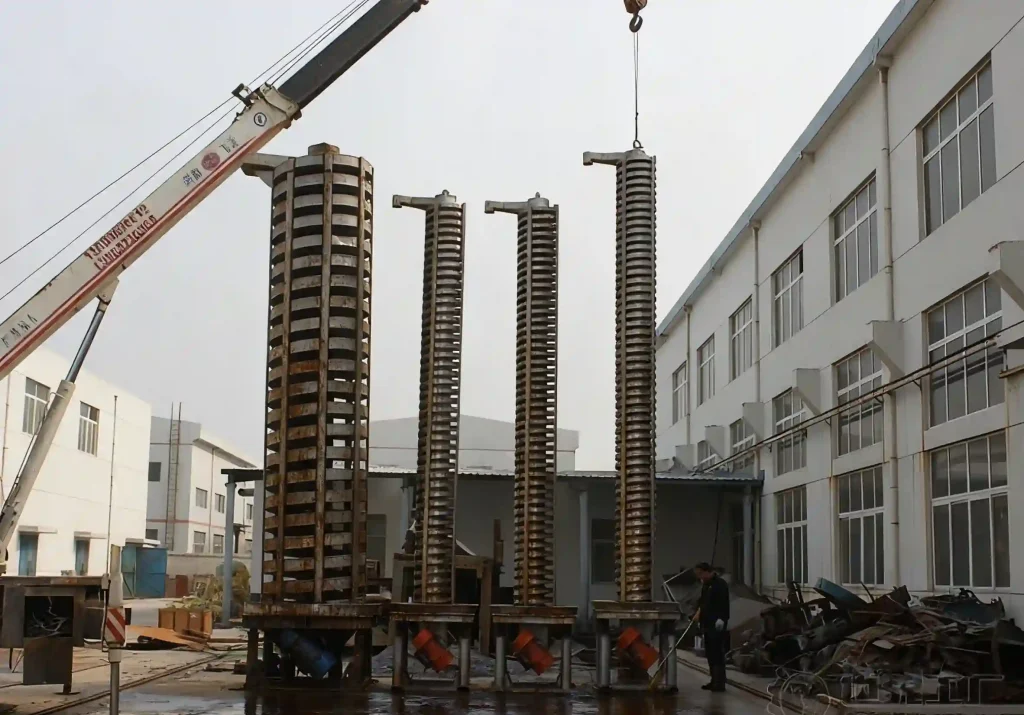
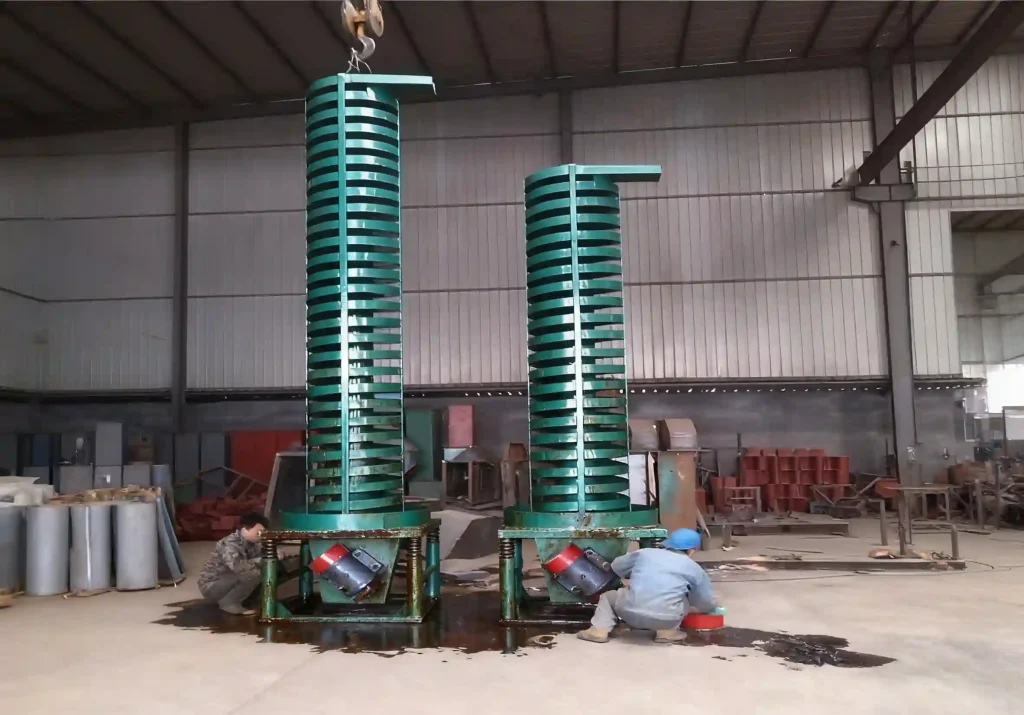
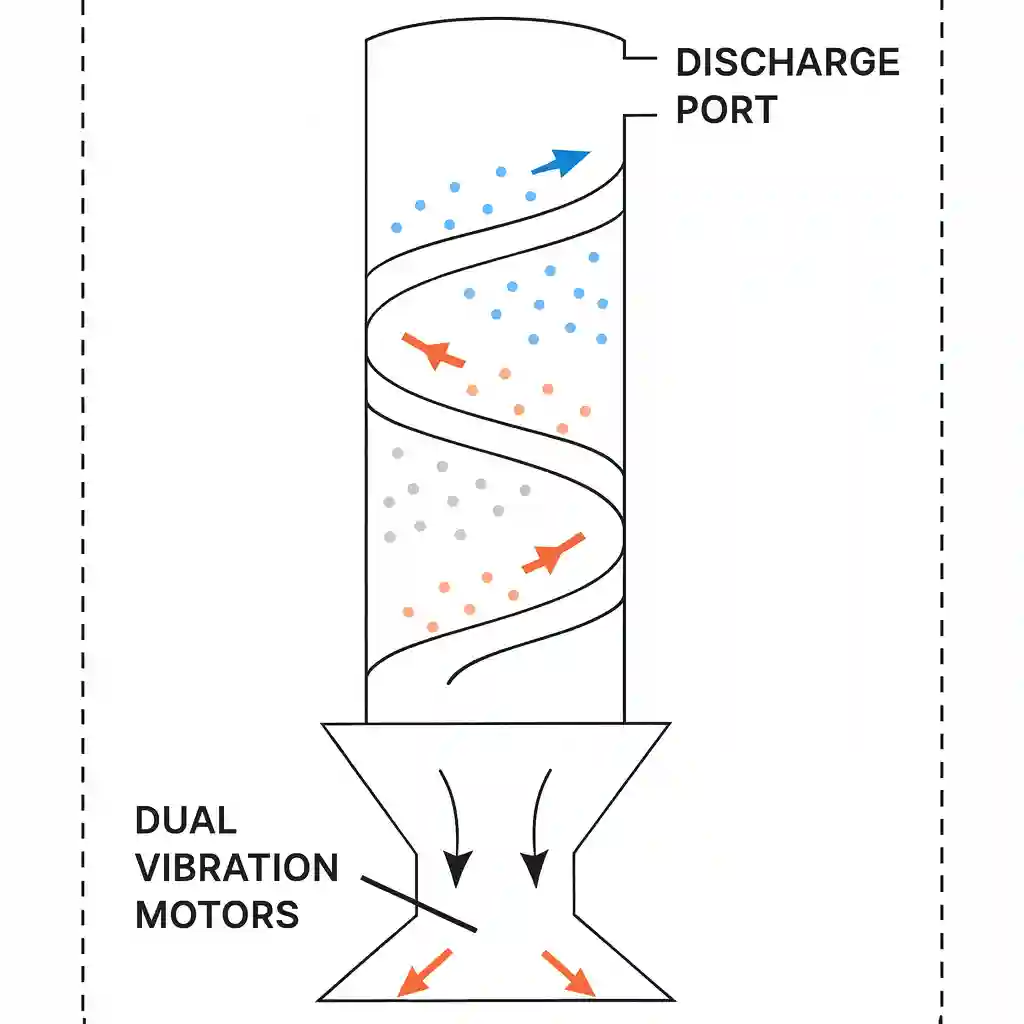
The Vertical Vibrating Screw Elevator is a conveying machine that uses synchronized vibration to move materials along a helical trough. It is capable of handling powders and granules up to 50 mm, achieving vertical transport with minimal degradation. With a capacity of 1–4 t/h, it features gentle material handling (<0.5% product breakage, SGS-verified), compact design, and low maintenance, making it suitable for continuous upward or downward conveying. The product is widely used in minerals, food, chemicals, and pharmaceuticals, including silica sand, grains, flour, polymer pellets, and pharmaceutical powders.
The Vertical Vibrating Screw Elevator is an efficient conveying device that uses synchronized vibration to transport powders and granules along a helical trough. Its compact design makes it easy to install and maintain, while occupying 50% less space compared to traditional bucket elevators. The device not only provides reliable vertical conveying with a capacity of 1–4 t/h, but also ensures gentle handling with less than 0.5% product degradation (SGS-verified), reducing material loss.
In addition, its bi-directional conveying capability allows both upward and downward transport in a single unit, increasing flexibility for different production lines. The absence of bearings and lubrication points in the contact zone minimizes maintenance costs and downtime. These features make it highly suitable for continuous operations in minerals, food, chemicals, and pharmaceuticals, ensuring stable, hygienic, and efficient material transfer.