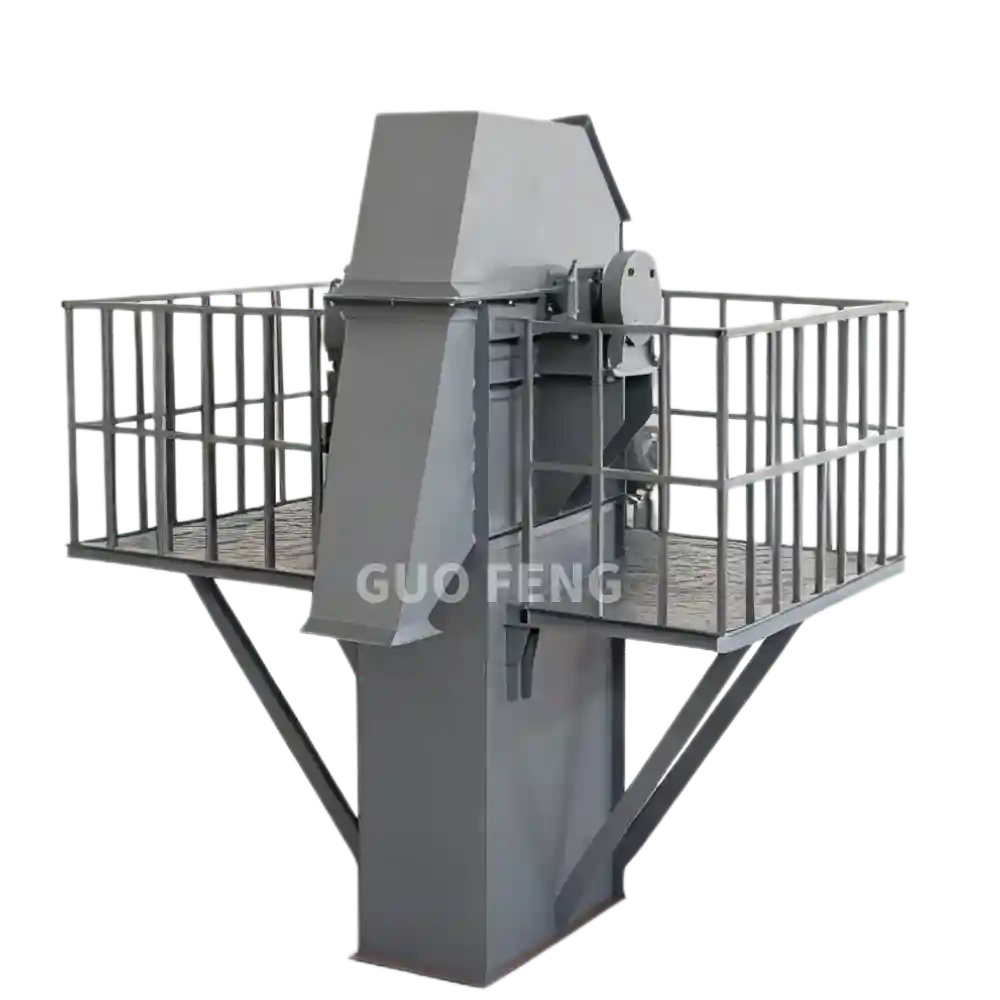
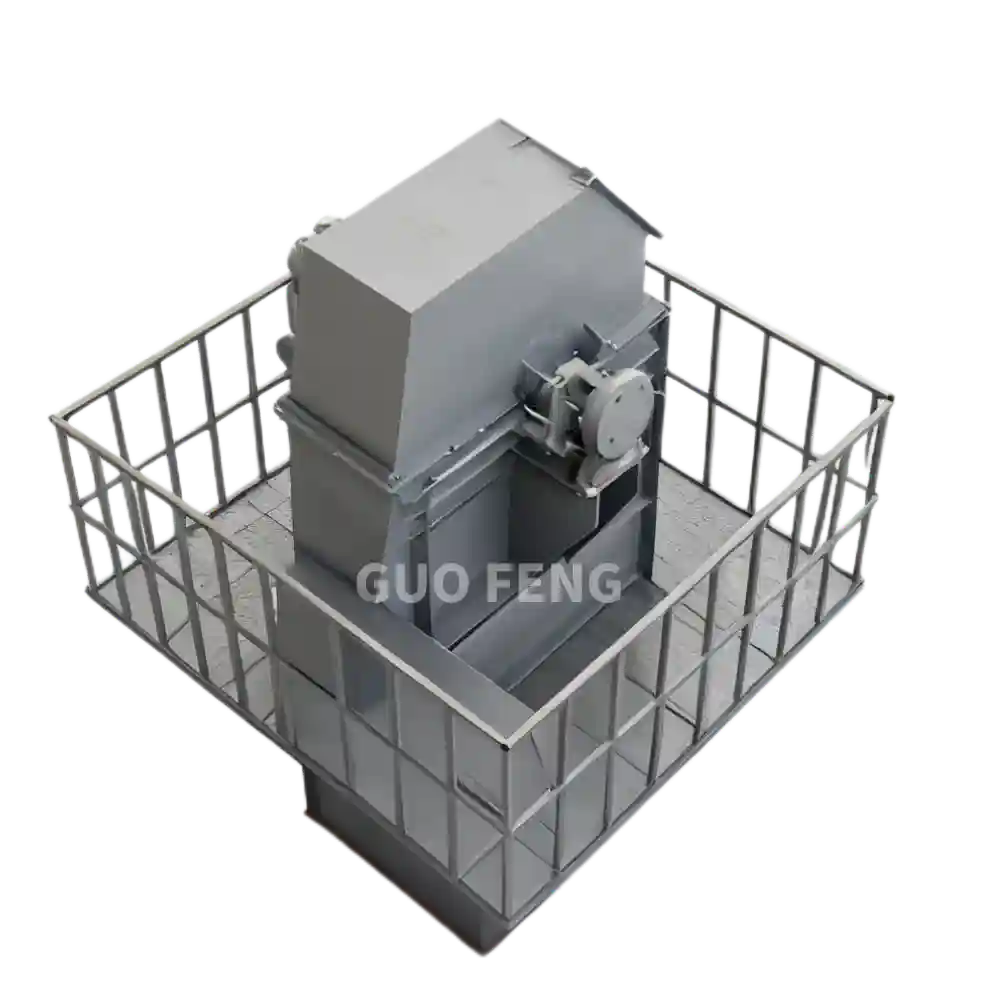
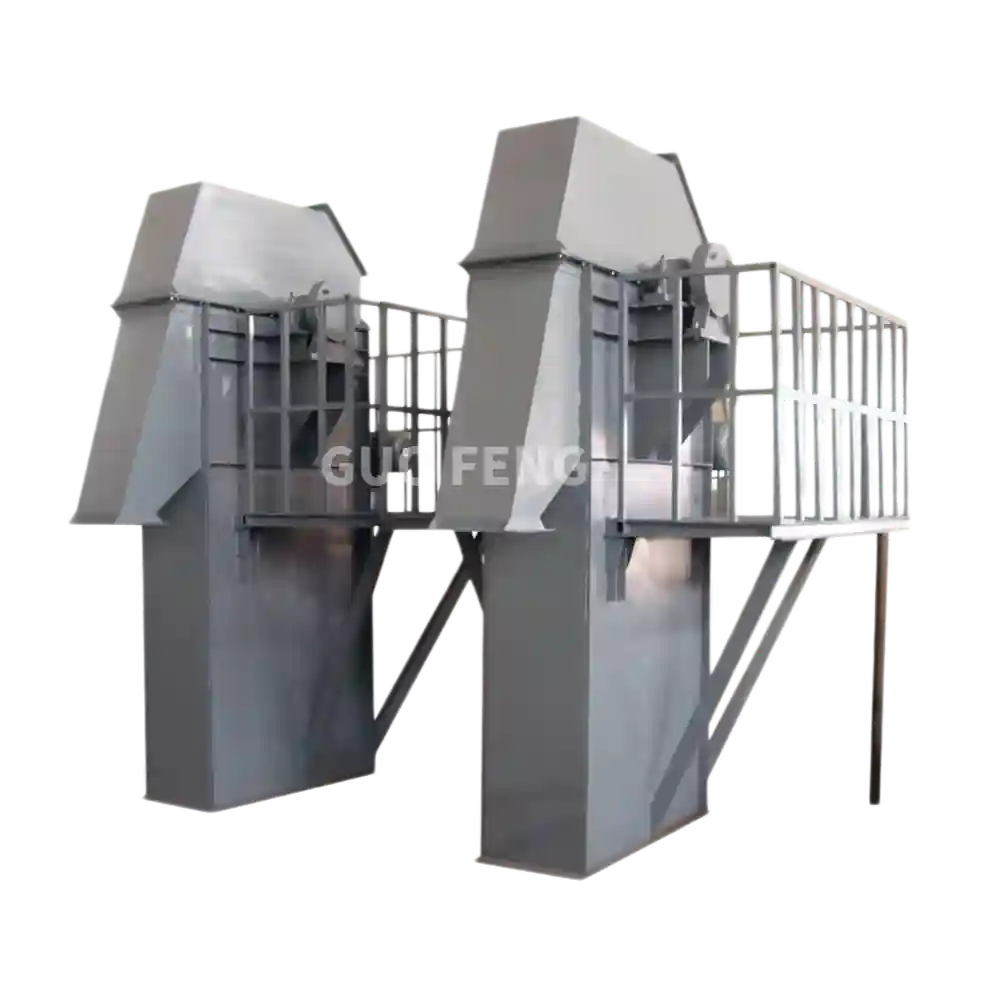
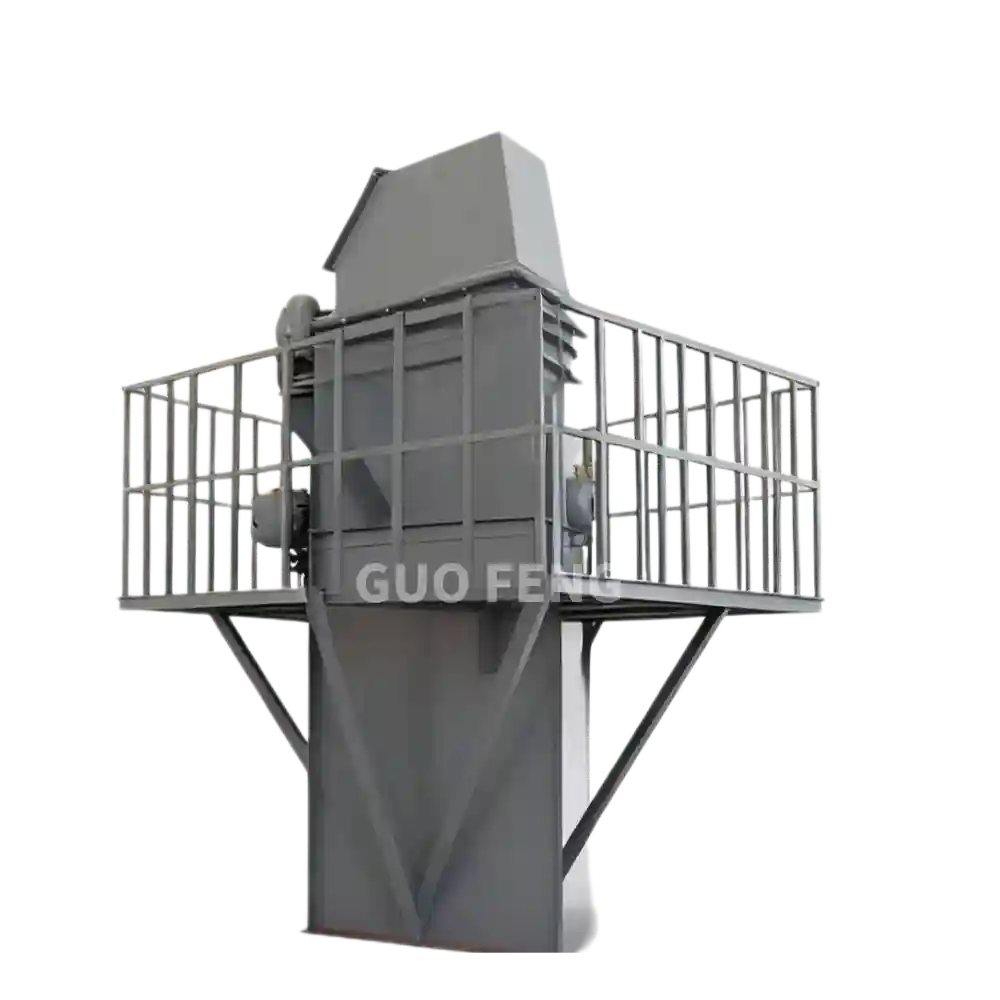
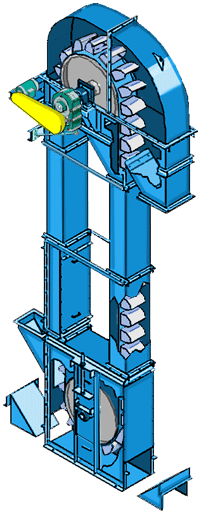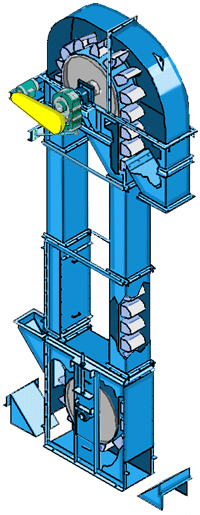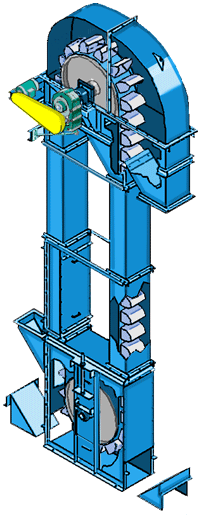
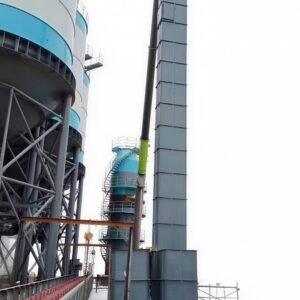
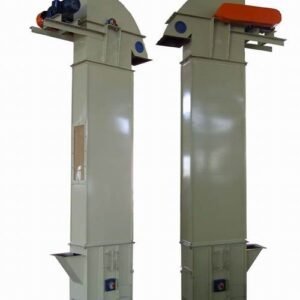
Application Areas: Heavy-duty vertical conveying of hot and abrasive bulk materials. Handles lumps up to 275 mm with continuous operation at 250°C. Widely used in cement plants (hot clinker), power stations (bottom ash), mining (copper/iron ore), and aggregates (limestone).
Particle Size Range
Operating Temperature
Capacity
Suitable for vertical conveying of lumps up to 275 mm and bulk materials at temperatures up to 250°C. Applicable materials include hot clinker, bottom ash, copper ore, iron ore, limestone, coal, and other abrasive or high-temperature bulk solids.
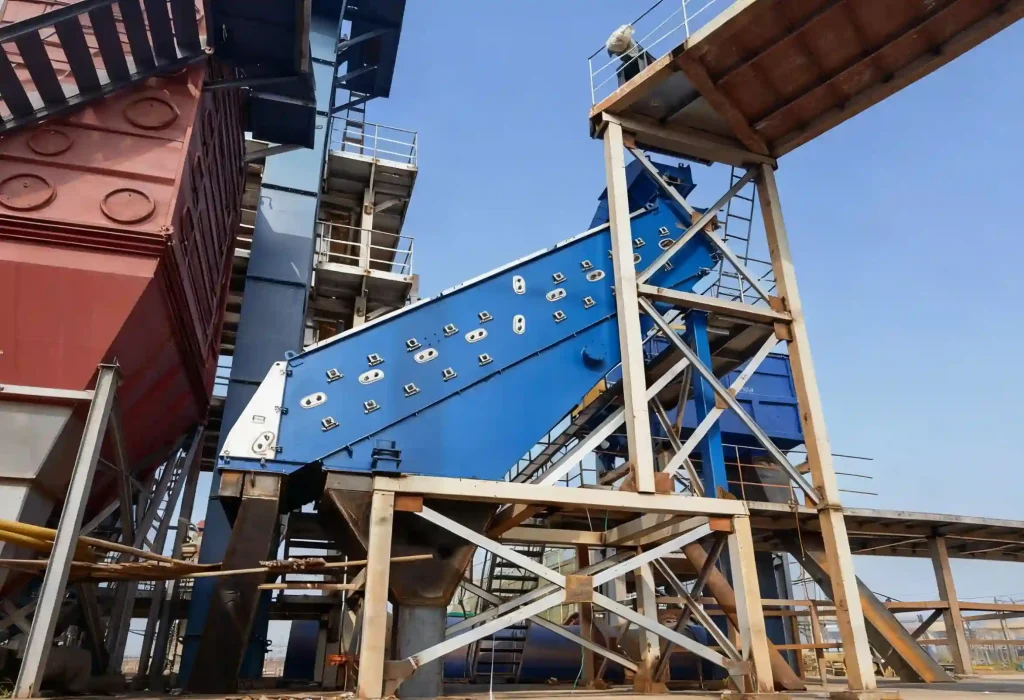
Widely used in cement plants (hot clinker conveying 200–250°C), power stations (bottom ash handling), mining (copper/iron ore hoisting), and aggregates industry (limestone lump transport). Designed for heavy-duty vertical bulk handling with high wear resistance and low maintenance.
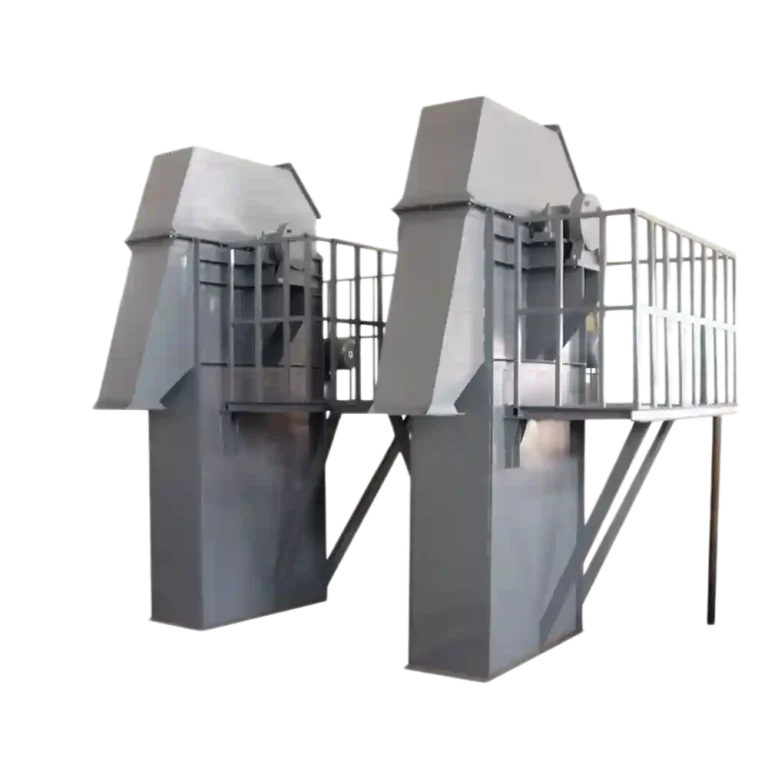
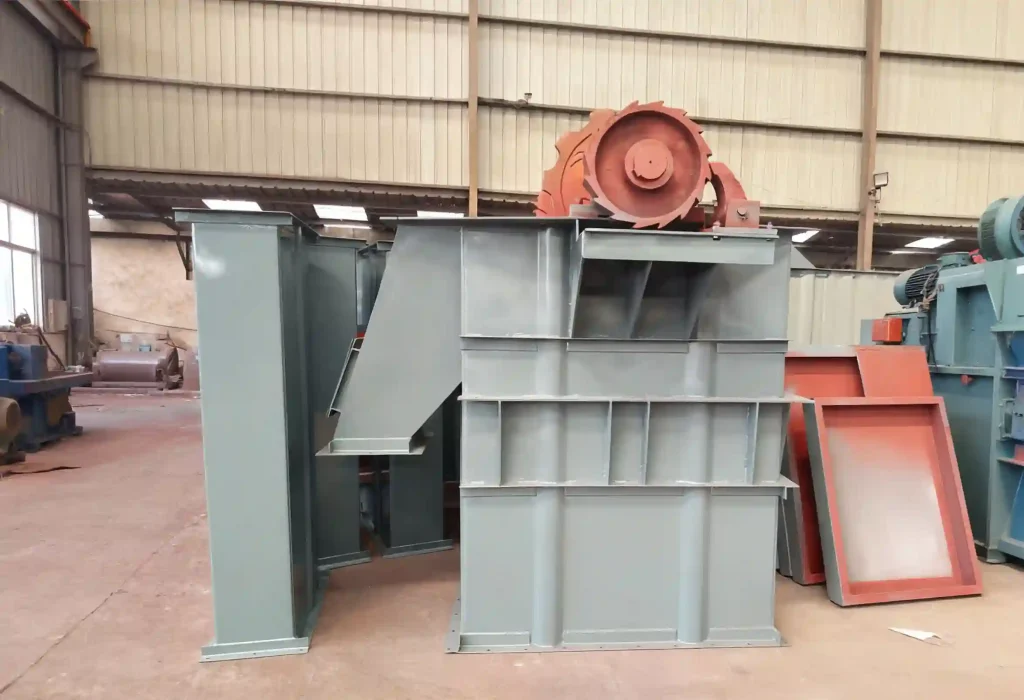
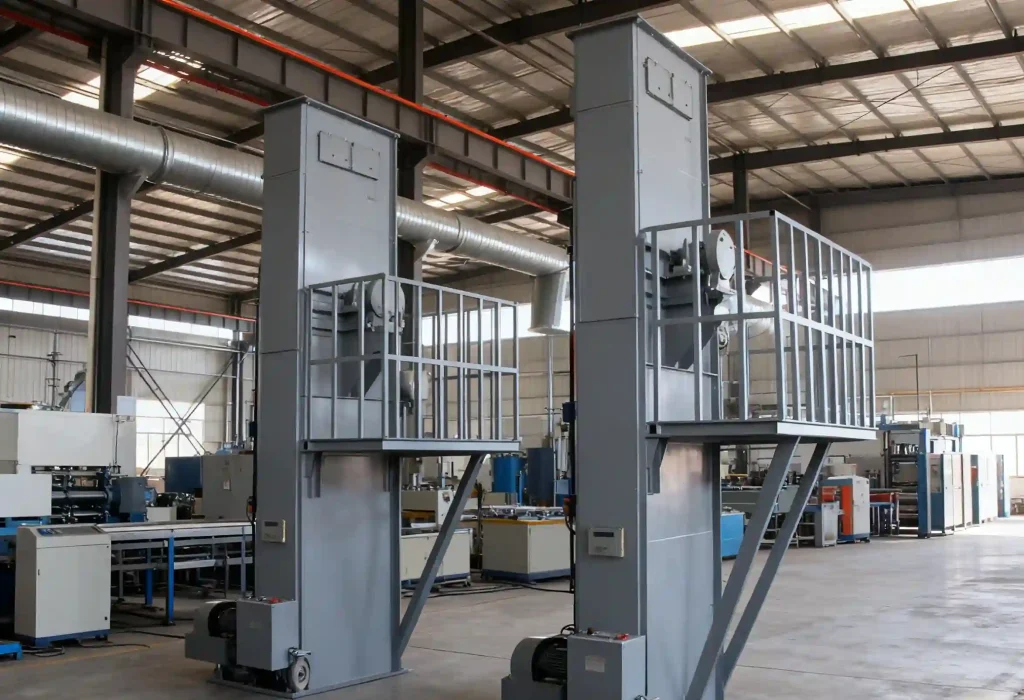
The NE Plate Chain Bucket Elevator is a heavy-duty vertical conveying machine certified under ISO 5050. It utilizes high-strength steel plate chains with deep buckets to transport bulk materials vertically at speeds of 0.3–0.5 m/s. The system is designed to handle lumps up to 275 mm and withstand continuous operating temperatures of up to 250°C, making it ideal for abrasive and high-temperature materials.
Featuring gravity discharge, it ensures smooth unloading with minimal material degradation. With Hardox 500 buckets and replaceable wear liners, DIN 7645-certified alloy steel chains, and a <0.5% annual downtime guarantee, it delivers reliable, low-maintenance performance. The NE series is widely applied in cement plants (hot clinker conveying), power stations (bottom ash handling), mining (copper/iron ore hoisting), and aggregates (limestone transport).
The NE Plate Chain Bucket Elevator is a heavy-duty vertical conveying solution designed for handling abrasive and high-temperature bulk materials. Equipped with Hardox 500 buckets and replaceable wear liners, it offers extreme abrasion resistance and ensures long service life even under harsh operating conditions.
Its DIN 7645-certified alloy steel chains deliver exceptional strength and stability, enabling reliable transport of lumps up to 275 mm at temperatures reaching 250°C. The gravity discharge design minimizes material degradation, while the dust-tight construction ensures clean operation and prevents spillage.
With a <0.5% annual downtime guarantee, the elevator requires minimal maintenance, significantly reducing operational costs. These advantages make it highly suitable for cement plants (hot clinker conveying), power stations (bottom ash handling), mining (ore hoisting), and aggregates (limestone transport).
The NE Plate Chain Bucket Elevator operates using high-strength steel plate chains with deep buckets fixed at intervals. During operation, the chain system drives the buckets to move vertically at a speed of 0.3–0.5 m/s, lifting bulk materials steadily. At the top, materials are discharged by gravity unloading, ensuring smooth flow and minimal degradation, even for lumps up to 275 mm.
This design provides reliable conveying of hot and abrasive materials, withstanding continuous temperatures of up to 250°C, making it ideal for cement clinker, coal, ores, and limestone.