INDUSTRIAL VACUUM CONVEYING SYSTEM

Application Areas: Closed and hygienic transfer of powders and granules. Widely used in pharmaceutical, food, chemical, and plastics industries. Suitable for API powders, milk powder, sugar, starch, polymer pellets, hazardous materials, etc. Meets GMP/FDA/ATEX standards, ensuring contamination-free and explosion-proof conveying.

0.5–5,000 kg/h

Transfer Capacity

Up to 30 m

Conveying Distance

99.9%

With Automatic Pulse Cleaning

1 33
60S Quick response
30 min Technical reply
24h design proposal
365 days to receive service needs
1 53
1 43
1 23
1 13

Applicable Materials

Suitable for conveying powders, granules, and bulk solids, including API powders, milk powder, sugar, starch, coffee, flour, chemical raw powders, polymer pellets, carbon black, etc. Ensures dust-free, hygienic, and contamination-free transfer.
Application Areas

Widely used in pharmaceutical, food, chemical, plastics, and new materials industries. Applicable for closed, hygienic, and explosion-proof powder conveying. Meets GMP/FDA/ATEX standards, ideal for automatic production lines.

Industrial Vacuum Conveying System

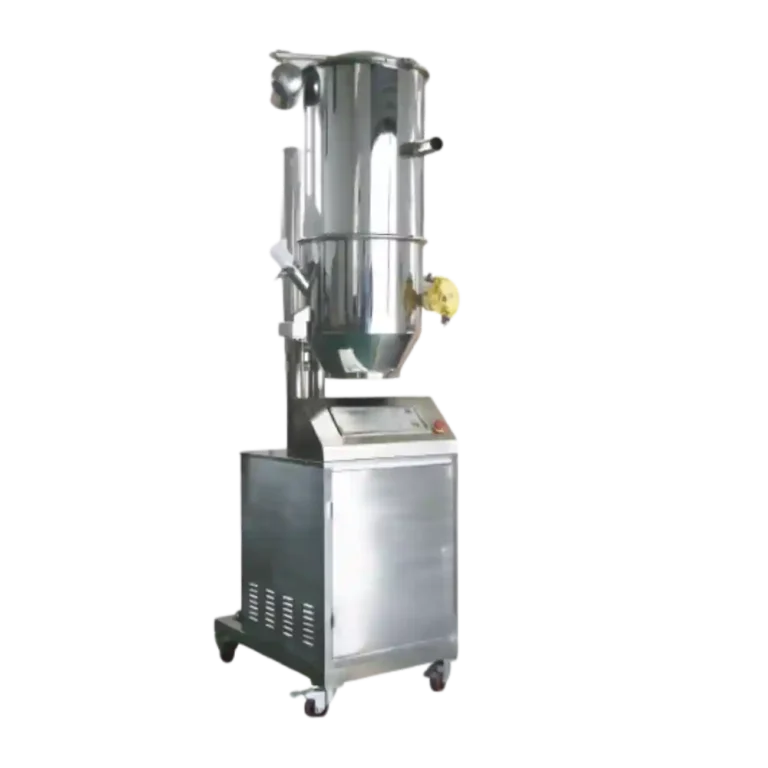
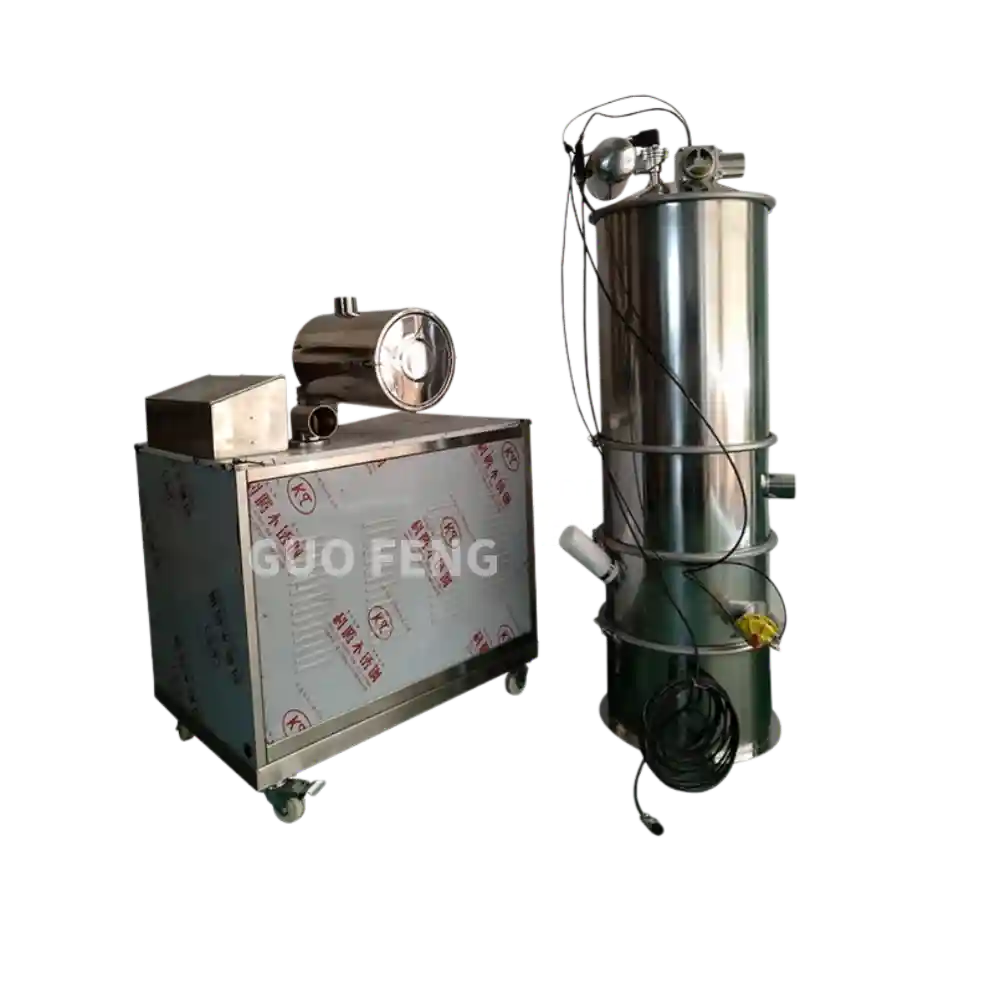
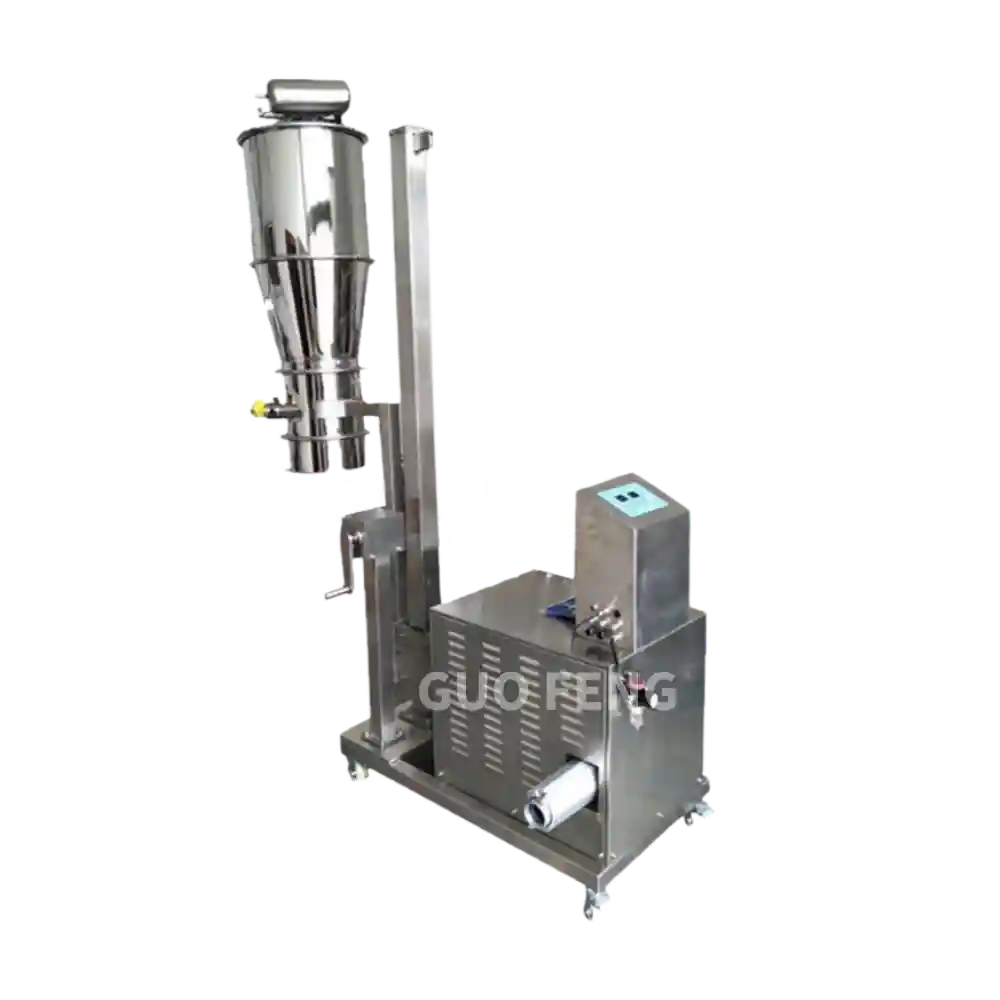
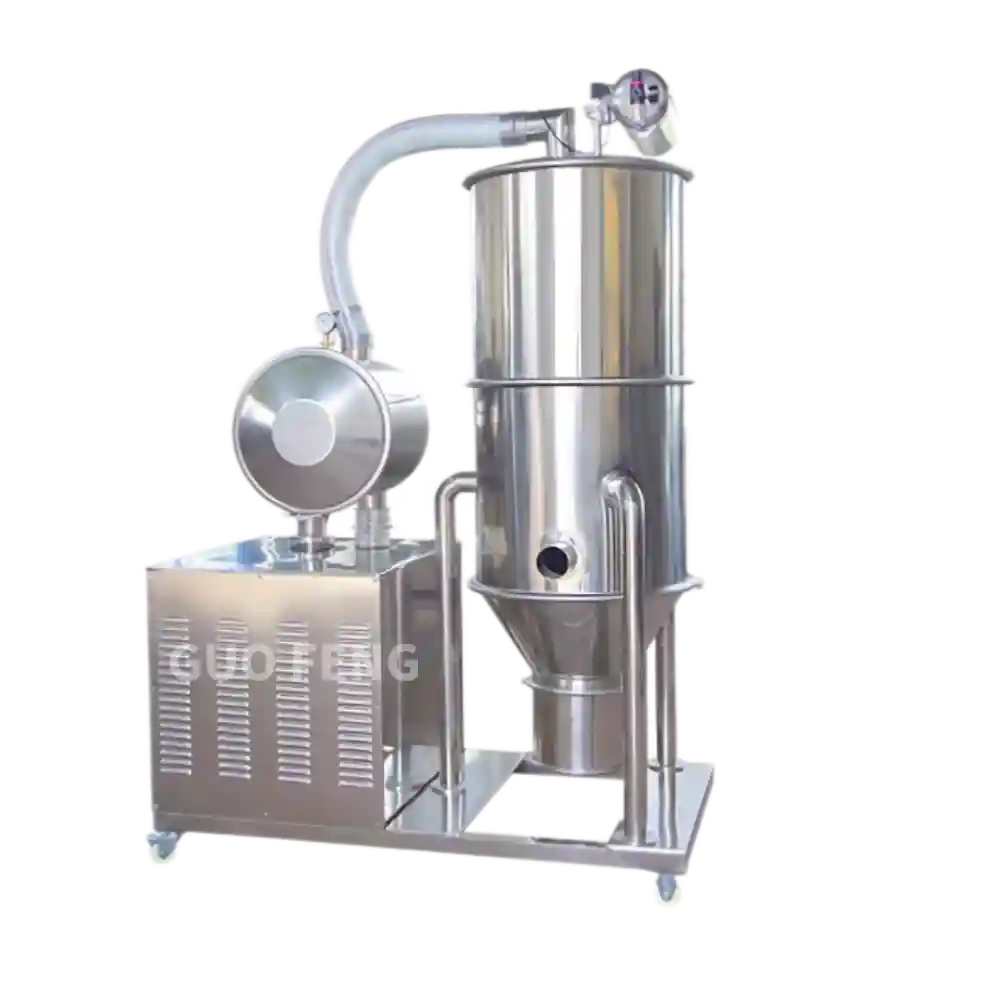
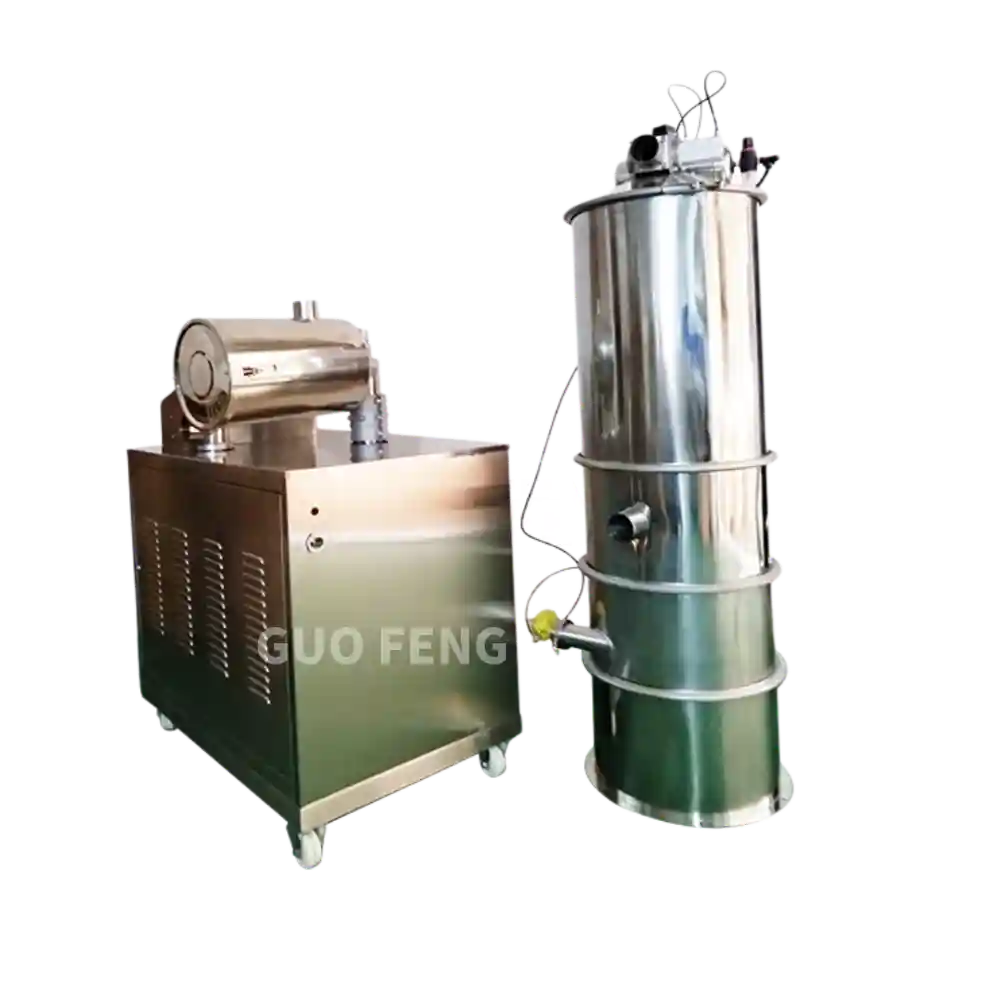
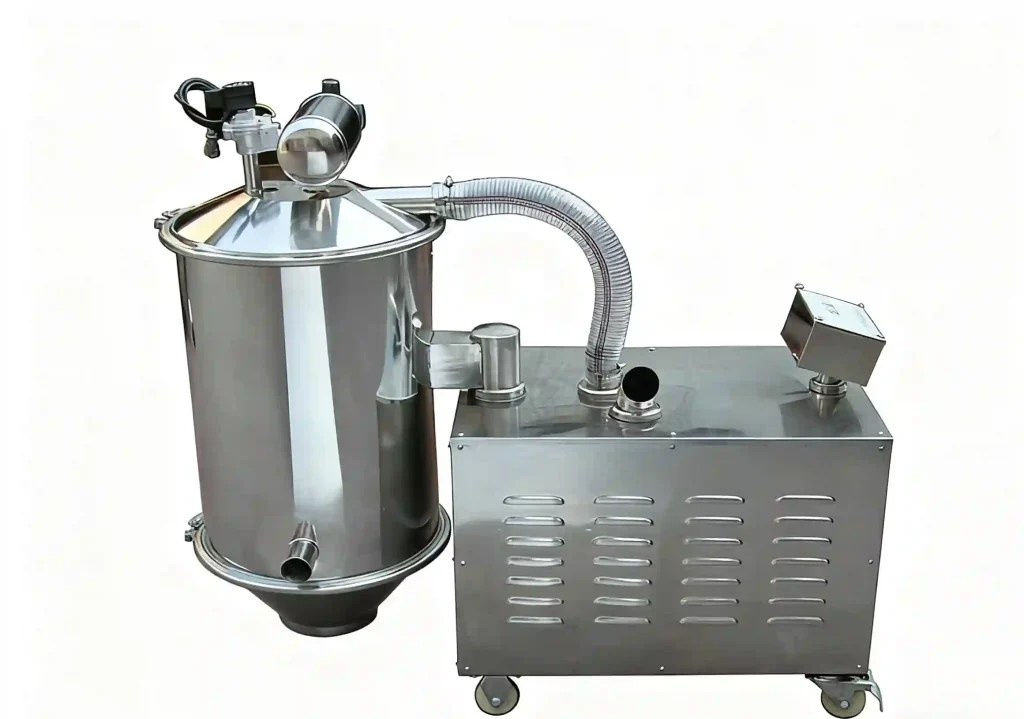
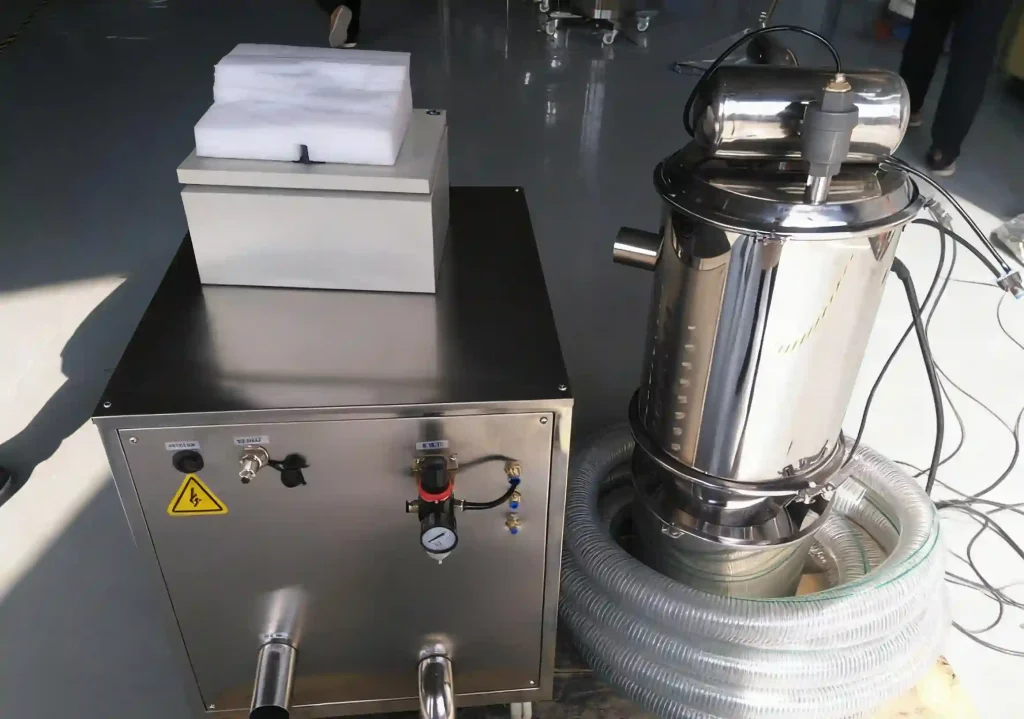
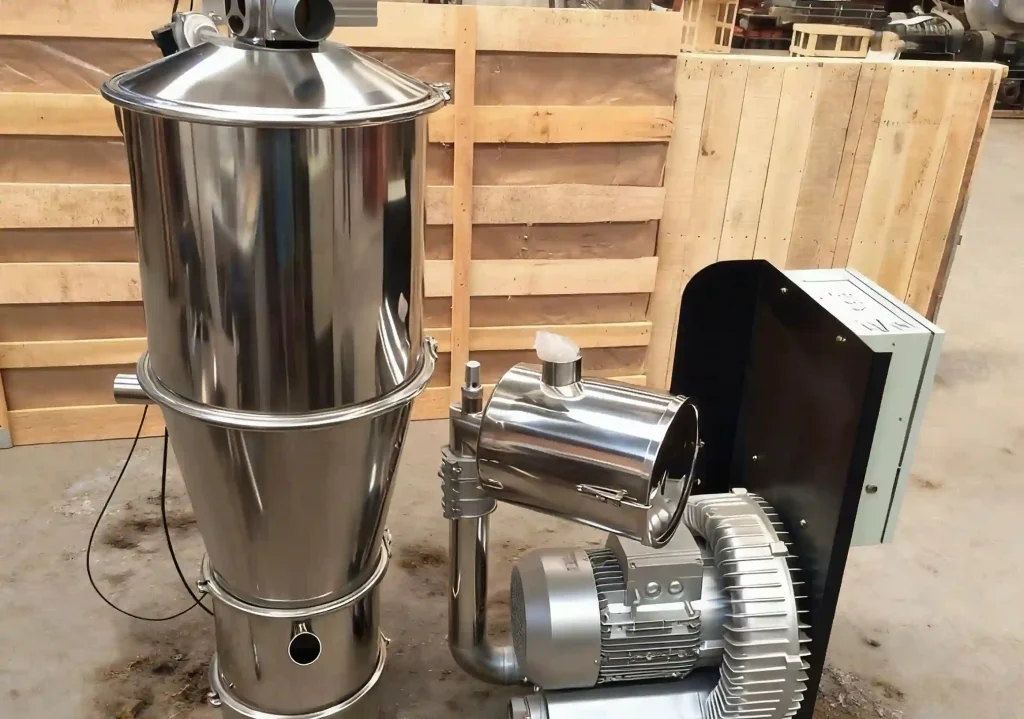
The Industrial Vacuum Conveying System is an advanced powder handling equipment that uses negative pressure air flow to transfer materials in a closed pipeline. It is capable of handling various powders, granules, and bulk solids with particle sizes ranging from micron-level to several millimeters. It features dust-free conveying, high efficiency, hygienic design, and easy maintenance, making it widely applicable in pharmaceutical, food, chemical, plastics, and new materials industries. The system ensures contamination-free transfer, meets GMP/FDA/ATEX standards, and is ideal for automatic continuous production lines.

图片比例调整
图片比例调整 1

Product Advantage

The Industrial Vacuum Conveying System is an efficient powder handling solution that uses negative pressure conveying technology to safely and cleanly transfer materials through closed pipelines. Compared with traditional mechanical conveying, it prevents dust pollution, material spillage, and cross-contamination, ensuring a clean and safe working environment.

Its simple modular design makes it easy to install, disassemble, and maintain, while providing strong conveying capacity for a wide range of powders and granules. The system offers higher efficiency, reduced labor intensity, and lower energy consumption, fully meeting GMP/FDA standards.

Additionally, it supports automatic feeding, continuous production, and flexible layout, making it widely applicable in pharmaceuticals, food, chemicals, plastics, and new material industries.

按比例修改图片 3
按比例修改图片 2

Applicable Feeding Materials

Have Any Questions!

Don't Hesitate To Contact Us AnyTime.

4ad2f911a7069ab904307736d31b2ccf1
Sand & Aggregates
ee2e567a28d71a4bd854a0dde3fa4fa91
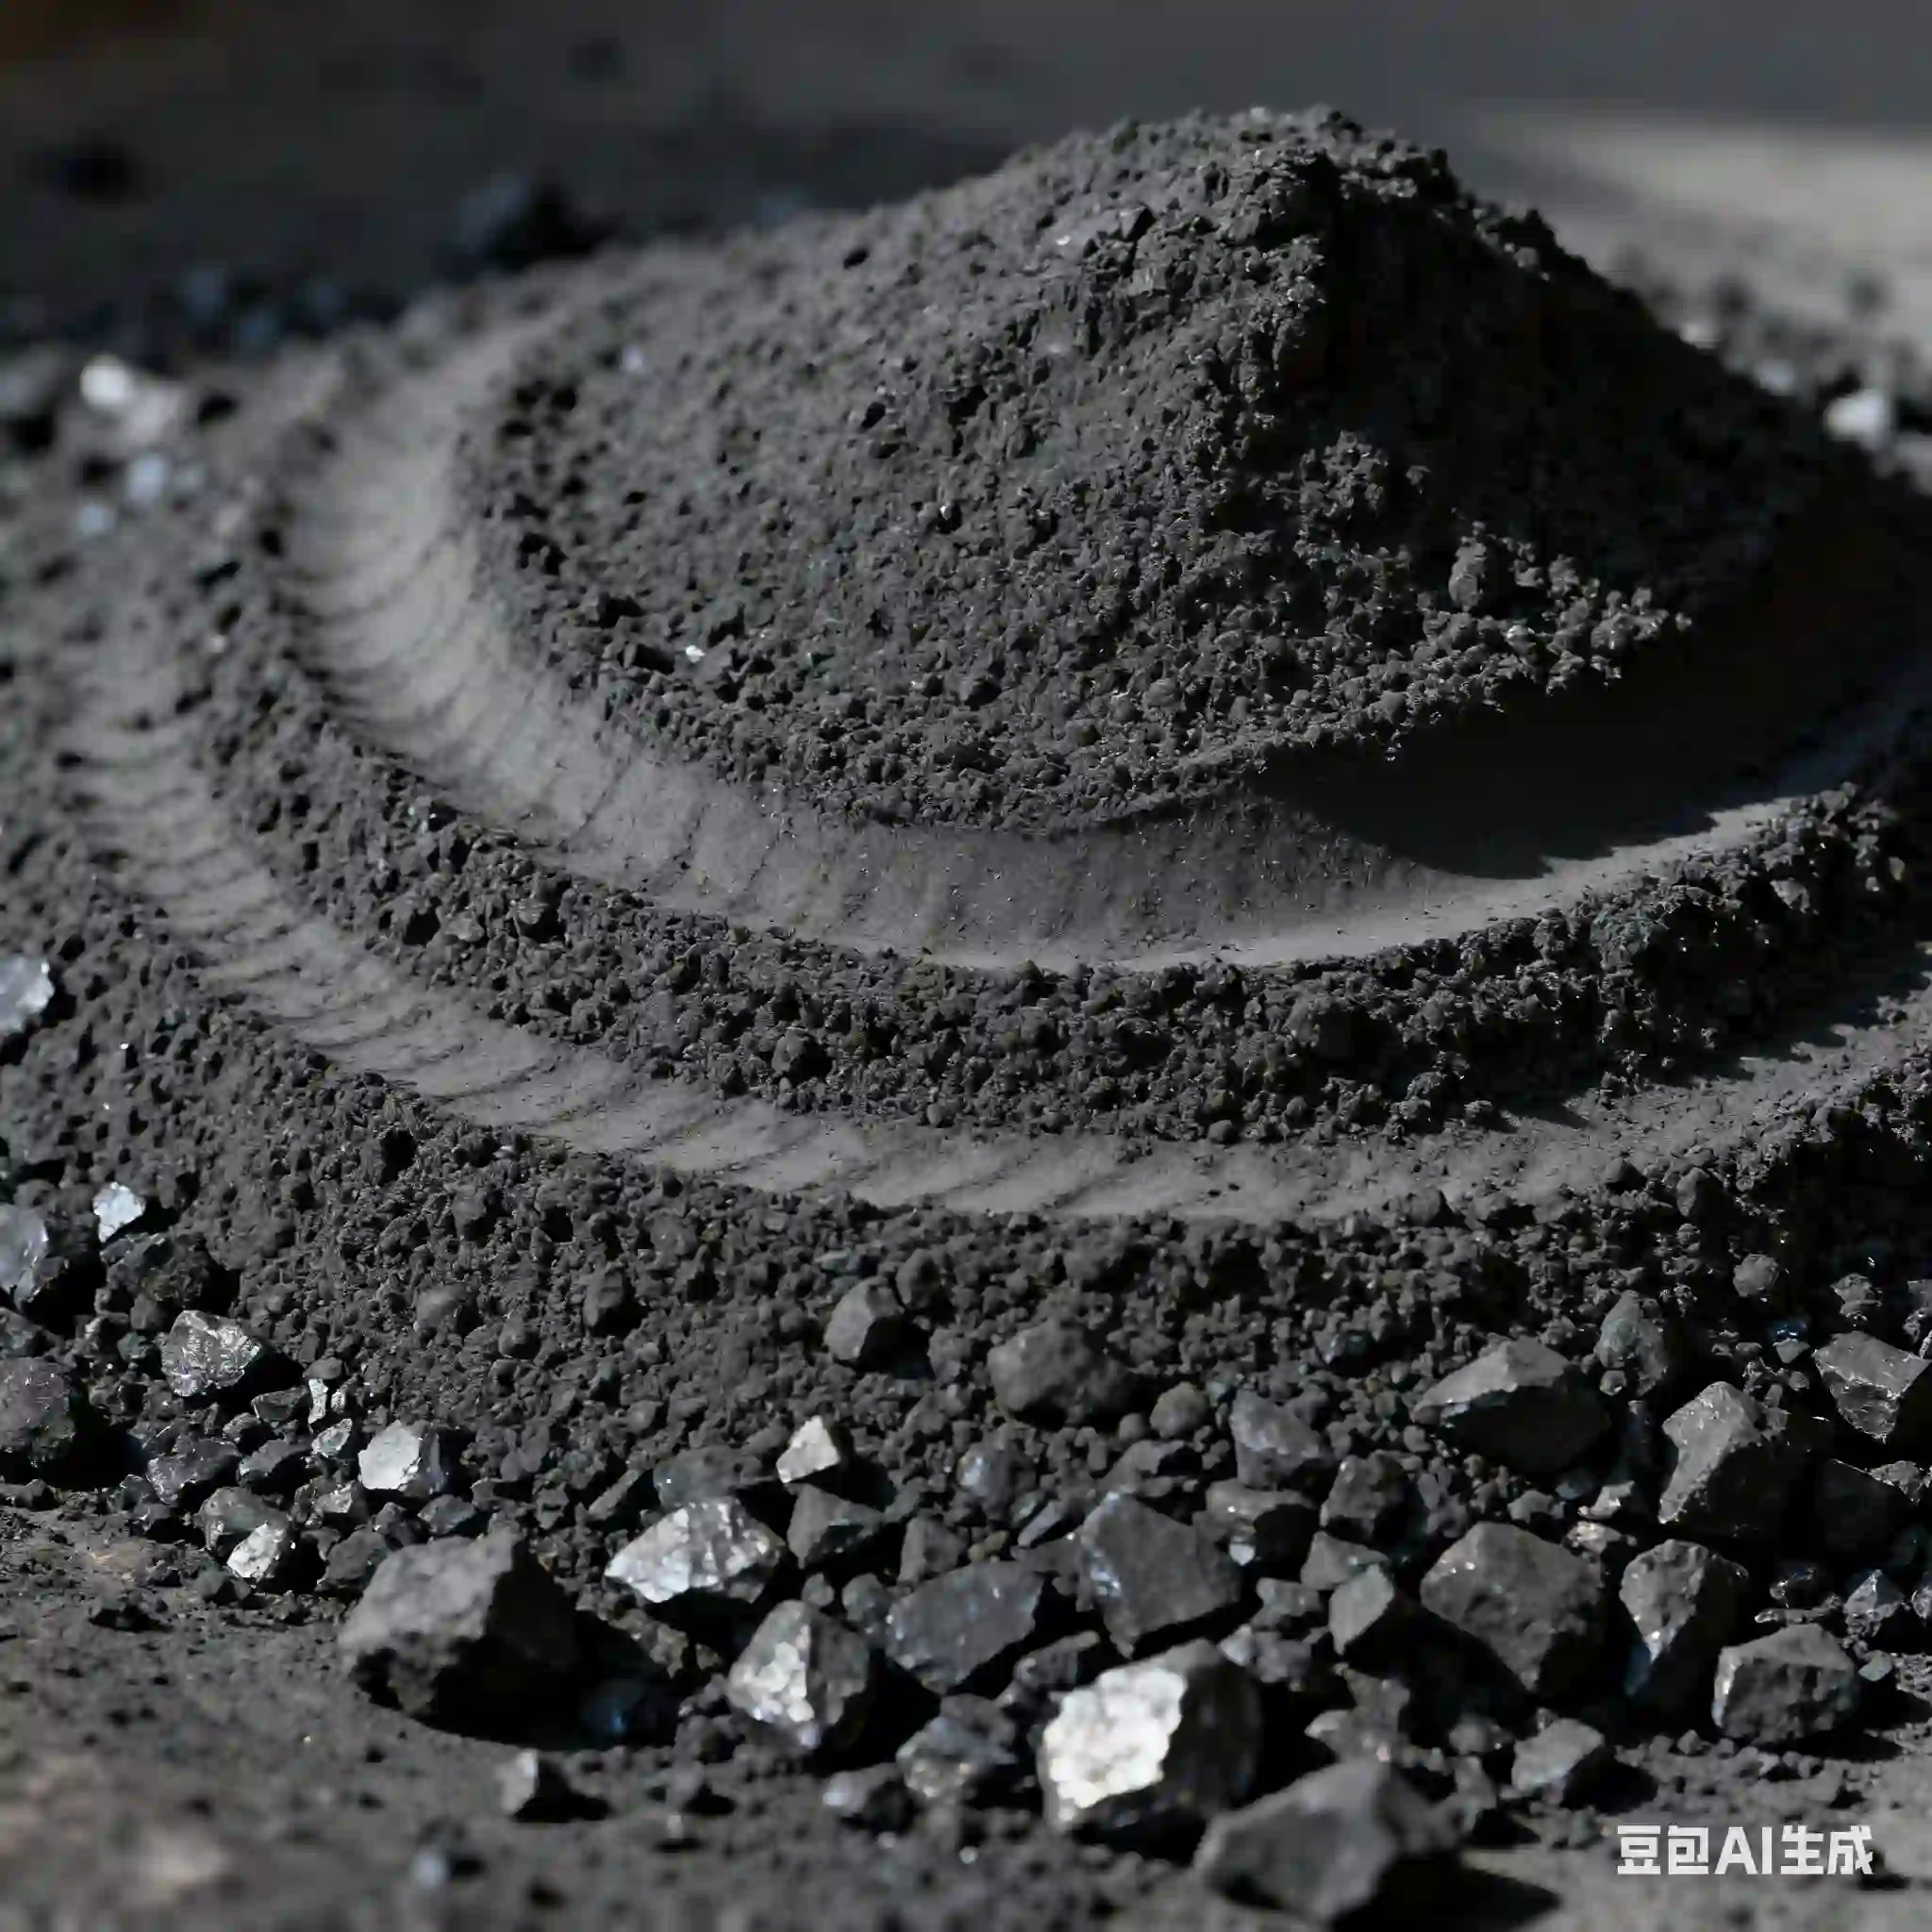
Coal
442fa53ceceb6a63c831184232a1158a1
Cement / Chemicals / Grain
5bcb14df8eb6c15f0e4e3fad91beefb21
Ore / Minerals

Working Principle

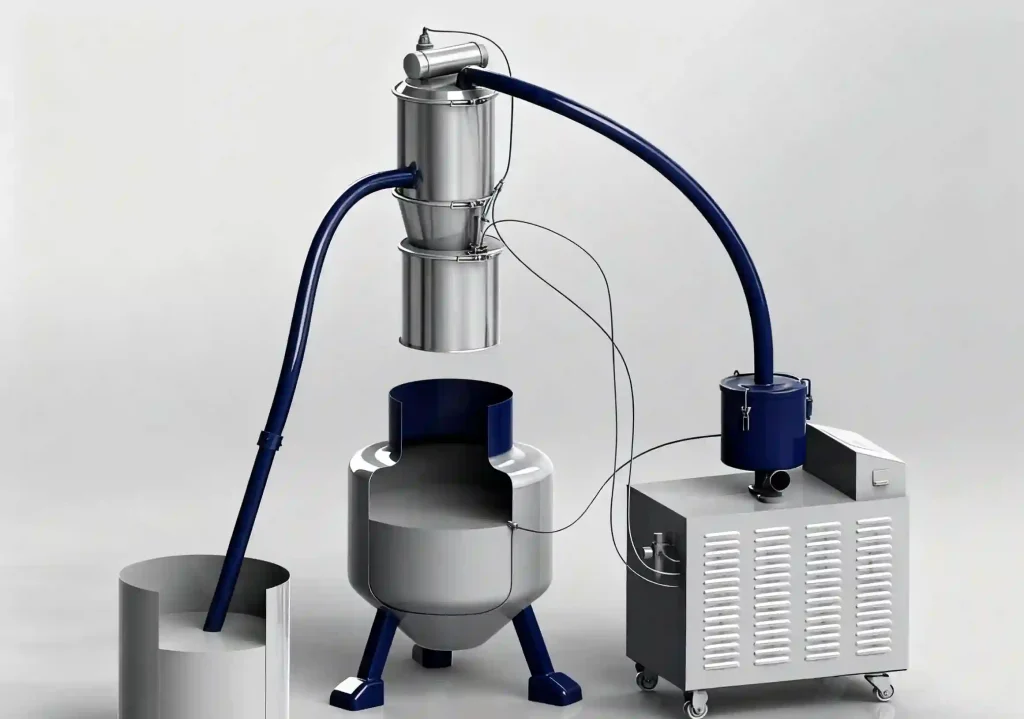
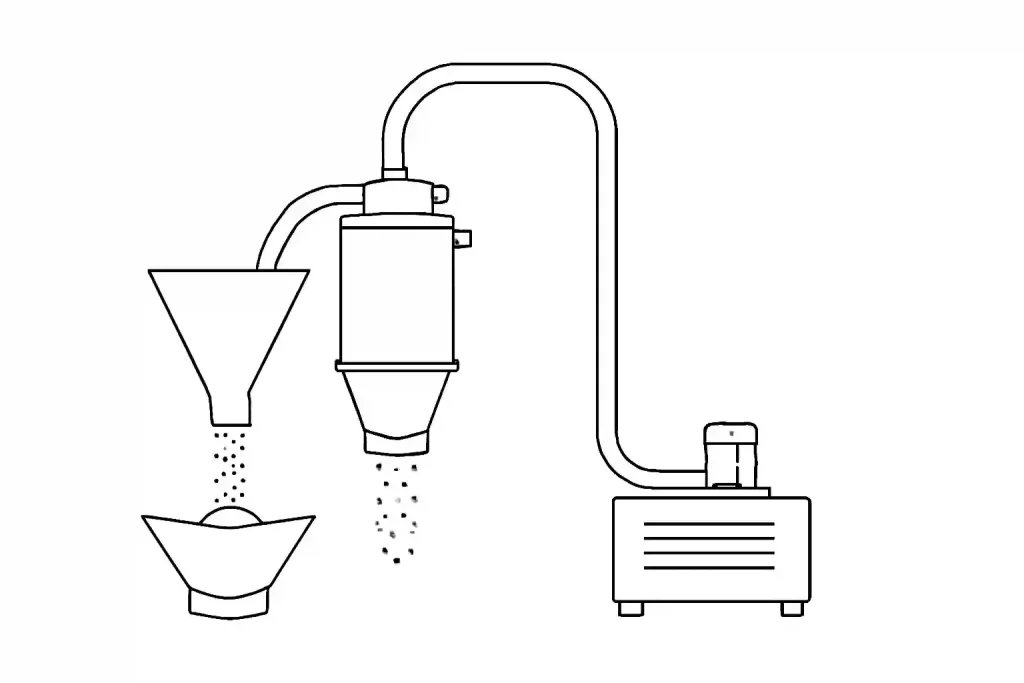
The industrial vacuum conveying system operates by creating a negative pressure environment within a sealed pipeline. Material is drawn into the system through a suction nozzle or feeding station, entrained in an airflow, and transported to the receiving container. During this process, dust and fine particles are filtered and collected to ensure a clean and contamination-free environment. The system provides enclosed, dust-free conveying, ideal for powders, granules, and bulk solids across industries such as food, pharmaceuticals, chemicals, and metallurgy.
47cbd2cfb60032a99543ca490d66f258

Specification

*The output will vary according to different materials, feed particle size and other factors

Blogs

© 2025Xinxiang City Leader Machinery Co., Ltd. All Rights Reserved.

Email WhatsApp
WhatsApp QR Code

扫码添加 WhatsApp

Message